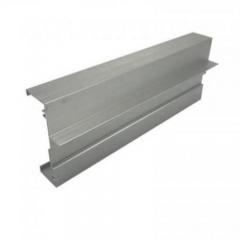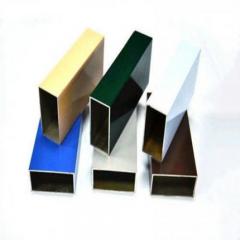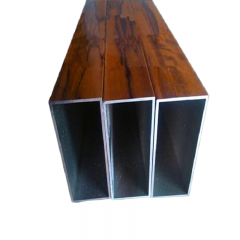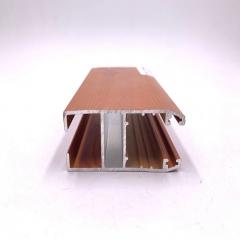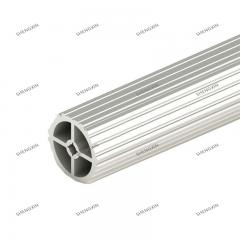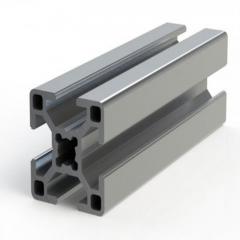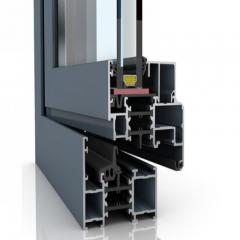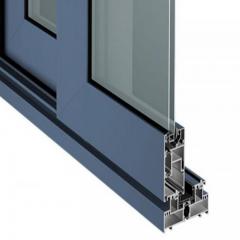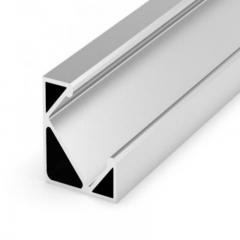
When you're building or upgrading a vessel, the materials you choose determine everything from durability to performance. Aluminum boat extrusions are precisely shaped aluminum profiles created specifically for marine construction, serving as the structural backbone and finishing elements of modern watercraft. These profiles range from heavy-duty hull components to decorative boat molding and protective aluminum extrusion trim that gives vessels their polished, professional appearance.
But what exactly makes these extruded profiles so essential to boat builders worldwide? It comes down to a manufacturing process that delivers remarkable consistency combined with material properties perfectly suited for life on the water.
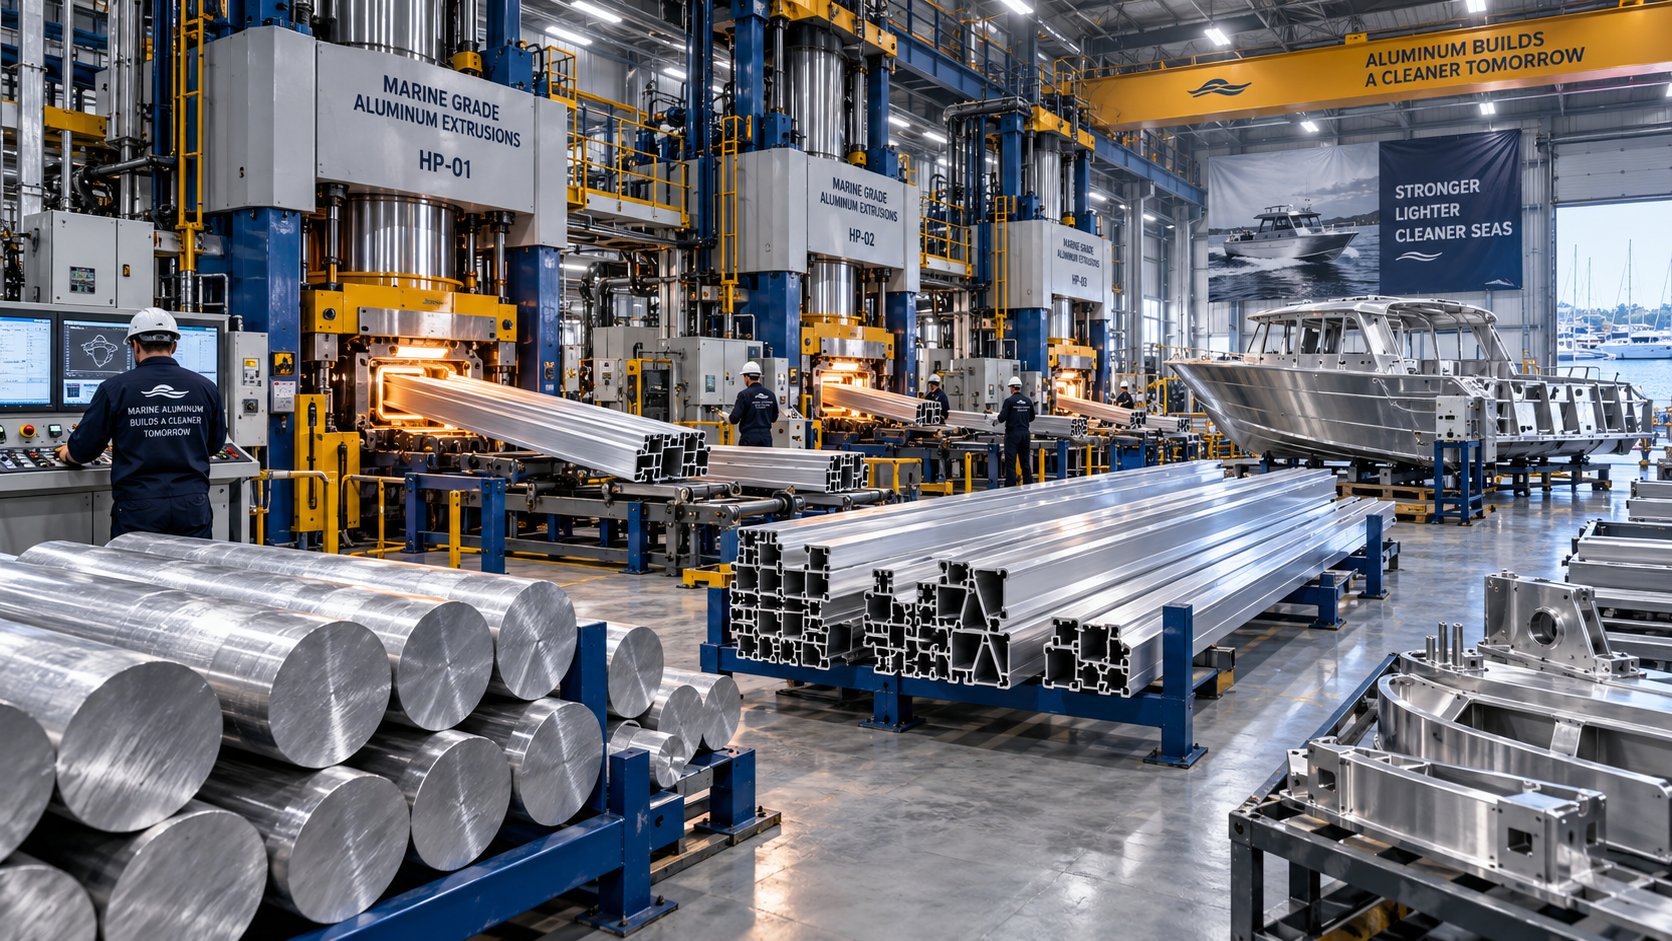
Imagine squeezing toothpaste from a tube - that's essentially how aluminum extrusion works, just with far more precision and pressure. The process begins with a cylindrical aluminum billet, which manufacturers preheat to temperatures between 400-500°C. This heating makes the metal malleable without melting it completely.
Once heated, the billet enters an extrusion press where a hydraulic ram applies up to 15,000 tons of pressure. This incredible force pushes the softened aluminum through a specially designed steel die - a shaped opening that determines the profile's cross-section. As the metal emerges, it takes on the exact shape of the die opening, whether that's a simple angle, a complex T-section, or custom boat molding designed for a specific application.
After exiting the press, the newly formed profile undergoes rapid cooling through water baths or fans. This "quenching" process locks in the material's properties. Finally, technicians stretch the profiles to correct any minor twists and cut them to specified lengths, typically between 8 and 21 feet. The result? Consistent, precise profiles ready for marine applications.
Why do experienced boat builders consistently choose extruded aluminum over steel, fiberglass, or wood? The answer lies in a unique combination of characteristics that address the harsh demands of marine environments:
These characteristics explain why aluminum has become the material of choice for everything from small fishing boats to military patrol vessels. The extrusion process ensures each piece maintains identical dimensions throughout its length - a consistency that simplifies assembly and guarantees predictable performance across your entire build.
You've learned how extruded profiles are made - now comes a critical decision that affects every aspect of your vessel's performance: which aluminum alloy should you specify? Not all aluminum is created equal, and choosing the wrong grade for your marine environment can lead to premature corrosion, structural weakness, or unnecessary expense.
Marine-grade aluminum alloys fall into two primary families, each engineered for specific applications. Understanding the differences between these series helps you match materials to components, whether you're sourcing structural hull sections or decorative aluminum boat trim for finishing touches.
The 5XXX series alloys use magnesium as their primary alloying element, creating exceptional corrosion resistance that makes them ideal for direct water contact. According to Howard Precision Metals, these wrought aluminum-magnesium alloys are often used for docks, boat lifts, structural shipbuilding, and offshore applications where saltwater exposure is constant.
The 6XXX series combines magnesium with silicon, delivering a different balance of properties. These alloys respond to heat treatment, allowing manufacturers to achieve specific strength levels through controlled processing. While still corrosion-resistant, 6XXX alloys truly excel in applications requiring superior surface finish and easier fabrication - making them perfect for aluminum boat trim molding and architectural elements.
Here's how the most common marine alloys compare across critical performance factors:
| Alloy Type | Tensile Strength Range | Corrosion Resistance | Weldability | Best Applications |
|---|---|---|---|---|
| 5052 | 31,000 - 38,000 psi | Excellent | Excellent | Fuel tanks, hull plating, general marine fabrication |
| 5083 | 40,000 - 46,000 psi | Exceptional | Very Good | Hull structures, military vessels, high-stress applications |
| 5086 | 35,000 - 42,000 psi | Exceptional | Very Good | Ship hulls, offshore platforms, pressure vessels |
| 6061-T6 | 42,000 - 45,000 psi | Very Good | Good (requires post-weld treatment) | Structural framing, near-water applications, aluminium t molding |
| 6063 | 27,000 - 33,000 psi | Very Good | Good | Decorative trim, railings, architectural elements |
Notice how 5083 delivers the highest strength among the 5XXX options? That's precisely why military and commercial shipbuilders specify it for hull construction. As noted by marine aluminum specialists, alloys 5083 and 5086 offer resistant hull plating that withstands seawater corrosion and impact damage while enabling weight reduction for improved speed and fuel efficiency.
When selecting between these families, consider your component's function. Structural elements requiring maximum corrosion protection? Choose 5XXX series. Trim pieces, railings, or components needing superior finish and easier machining? The 6XXX series delivers better results.
Here's something many boat builders overlook: the environment where your vessel operates dramatically affects alloy selection. Saltwater presents far more aggressive corrosion challenges than freshwater, and this distinction should guide your material choices.
In freshwater applications, most marine-grade alloys perform admirably with minimal maintenance. The 6XXX series alloys, including 6061 and 6063, provide more than adequate corrosion resistance for lakes, rivers, and reservoirs. Their easier machinability and superior surface finish make them cost-effective choices when extreme corrosion resistance isn't the primary concern.
Saltwater changes everything. The chloride ions in seawater accelerate corrosion and can cause pitting in alloys not specifically designed for constant salt exposure. For vessels operating in coastal waters, open ocean, or brackish environments, the 5XXX series becomes essential for any component with direct water contact.
Consider these environment-specific guidelines:
Why do military specifications consistently call for 5083? Beyond its exceptional saltwater resistance, this alloy maintains structural integrity under extreme stress conditions. According to Protolabs, the 5XXX series provides good stress-corrosion cracking resistance - critical for vessels that may encounter impact, vibration, or rapid pressure changes during operation.
One important note about welding: 6061 can experience weakening in heat-affected zones during welding, potentially requiring post-weld treatment to restore full strength. The 5XXX alloys generally maintain better properties after welding, making them simpler to fabricate for structural marine applications.
Understanding these alloy differences positions you to make informed decisions - but selecting the right material is only part of the equation. Matching your chosen alloy to the correct extrusion profile ensures each component performs its intended function flawlessly.
You've selected your alloy - now comes the next critical decision: which profile shape matches each component on your vessel? Think of extrusion profiles like puzzle pieces. The right shape fits perfectly, distributes stress efficiently, and simplifies installation. The wrong choice? You're left with awkward fabrication workarounds, unnecessary weight, or compromised performance.
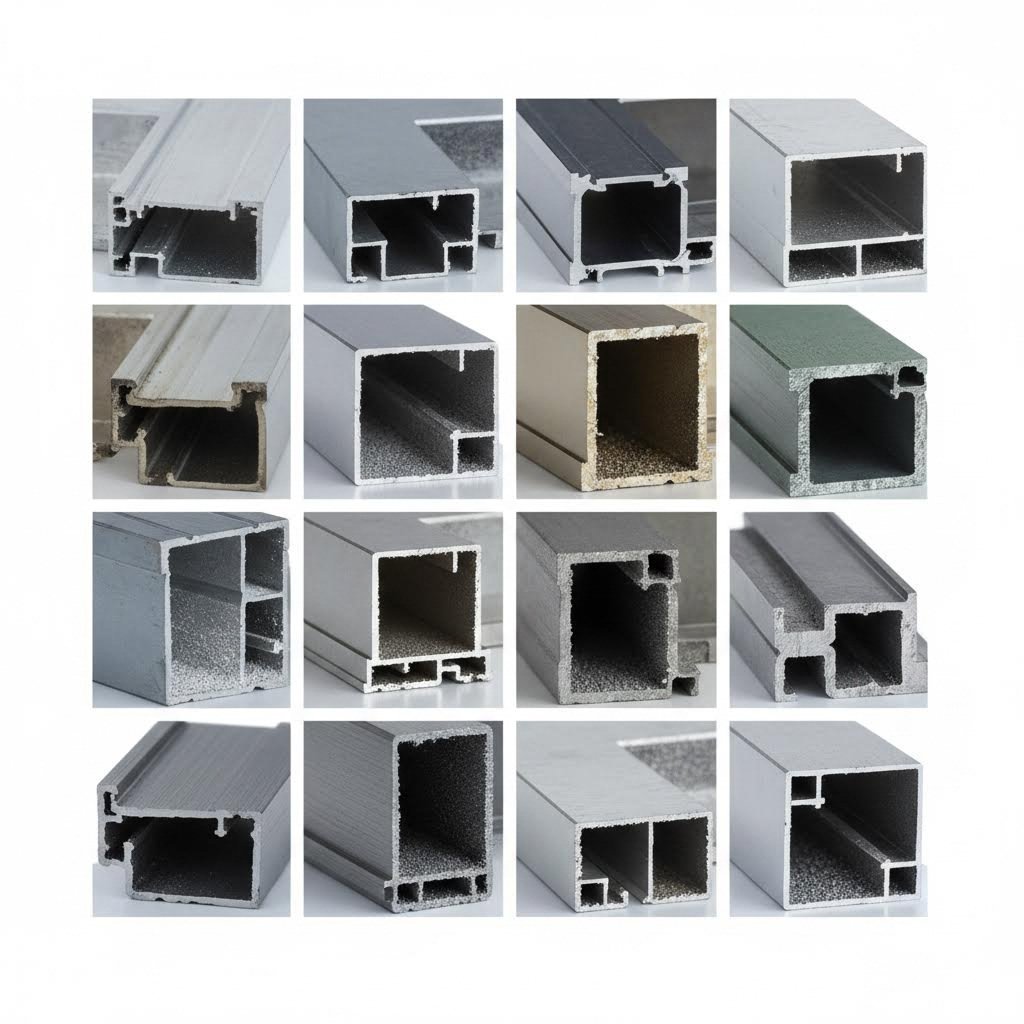
Marine extrusion profiles generally fall into three categories: standard profiles, special profiles, and customized profiles. Understanding when each category makes sense helps you balance cost, availability, and performance for your specific build.
Standard profiles include simple geometric shapes manufactured in common dimensions. These off-the-shelf options offer the lowest cost and fastest availability - ideal when your design accommodates conventional shapes.
Special profiles feature specific shapes and dimensional tolerances engineered for naval applications. They're manufactured to meet marine-specific requirements while remaining catalogued products available without custom tooling.
Customized profiles transform your technical drawings into finished extrusions. When standard options don't meet your needs, custom die development creates profiles matching exact specifications - though this requires tooling investment and longer lead times.
Structural components demand profiles engineered for strength, stress distribution, and efficient assembly. Here's where profile geometry directly impacts vessel performance and longevity.
When selecting structural profiles, dimensional consistency matters enormously. A stringer that varies even 1/16-inch along its length creates fitting nightmares during assembly. Quality extruders maintain tight tolerances - typically ±0.012 inches for wall thickness and ±0.024 inches for major dimensions - ensuring your components align properly throughout the build.
Consider your welding approach when choosing profile thickness. Thinner walls (under 1/8-inch) require more precise heat control during welding to prevent burn-through or distortion. Heavier profiles tolerate broader welding parameters but add weight. Most recreational boat builders find the sweet spot between 1/8-inch and 3/16-inch wall thickness for primary structural extrusions.
While structural profiles handle the heavy lifting, trim extrusions protect edges, cover joints, and give your vessel its finished appearance. These components see constant exposure to UV, saltwater spray, and physical contact - making profile selection equally important for durability and aesthetics.
Specialty profiles push beyond standard geometric shapes into application-specific designs:
How do profile dimensions affect your finished vessel? Consider rub rails as an example. A profile that's too small won't adequately protect against dock impact. One that's too large creates unnecessary drag and adds weight. Most recreational boats between 16 and 24 feet use rub rails measuring 1.5 to 2.5 inches in height, scaled to hull depth and expected use conditions.
For trim applications, profile width should match or slightly exceed the surfaces being covered. Boat molding trim that's too narrow leaves visible gaps; excessive width wastes material and looks disproportionate. When in doubt, order samples before committing to production quantities - the few dollars spent on samples prevents costly ordering mistakes.
Surface finish quality also varies between profile categories. Standard structural extrusions typically feature mill finish adequate for painted or hidden applications. Decorative trim often requires upgraded surface quality - look for profiles specifically designated for visible applications when aesthetics matter.
With your alloy selected and profiles matched to components, the next consideration is how different vessel types influence these choices at a systems level - from private recreational boats to commercial and military applications.
You've selected your alloy and matched profiles to components - but how do these choices change based on the type of vessel you're building? A weekend fishing boat faces different demands than a commercial trawler or military patrol craft. Understanding how vessel classification influences extrusion specifications helps you make smarter decisions from the start.
Whether you're a DIY builder tackling your first aluminum skiff or a professional fabricator bidding on commercial projects, matching specifications to vessel requirements prevents costly over-engineering or dangerous under-specification. Let's break down what each vessel category demands.
Recreational boats represent the broadest category, ranging from 12-foot jon boats to 40-foot cruisers. What unites them? Owners prioritize value, appearance, and reasonable longevity without the extreme durability requirements of commercial operations.
For most private vessels operating in freshwater, 6061-T6 structural extrusions paired with 6063 decorative trim deliver excellent performance at moderate cost. These alloys machine beautifully, accept anodizing and powder coating readily, and provide more than adequate corrosion resistance for lake and river use.
Saltwater recreational boats require upgraded specifications. Hull-contact components should shift to 5052 or 5086 alloys, while above-waterline trim can remain 6XXX series with appropriate surface protection. Many builders use rv aluminum trim molding and aluminum camper trim profiles for interior finishing - these readily available extrusions offer cost savings when marine-specific aesthetics aren't required.
Dimensional tolerances for recreational builds typically follow standard commercial specifications. Most DIY builders work successfully with tolerances of ±0.015 inches on wall thickness and ±0.030 inches on major dimensions. Tighter tolerances increase cost without proportional benefit for typical recreational applications.
Commercial vessels operate differently. Fishing boats, ferries, and workboats accumulate thousands of operating hours annually, facing constant saltwater exposure, heavy loading, and demanding maintenance schedules. These conditions demand upgraded specifications throughout.
Military applications push requirements further still. Naval vessels must withstand combat conditions, including shock loads from nearby explosions, extended deployments without maintenance access, and extreme reliability requirements. This explains why military specifications consistently call for 5083 alloy with stringent quality certifications.
Quality standards become critical at this level. The major certification bodies include:
The following matrix consolidates vessel types with their typical extrusion specifications:
| Vessel Type | Typical Alloy Selection | Common Profile Types | Surface Treatment Needs | Certification Requirements |
|---|---|---|---|---|
| Freshwater Recreational | 6061-T6 structural, 6063 trim | Standard angles, channels, J-molding | Mill finish or powder coating | None required; ASTM B221 recommended |
| Saltwater Recreational | 5052/5086 hull, 6063 trim | Heavy-wall channels, D-shaped rub rails | Anodizing or marine-grade powder coat | ASTM B221; manufacturer certification |
| Commercial Fishing | 5083 throughout | I-beams, heavy T-sections, reinforced channels | Hard anodizing or PVDF coating | ABS or Lloyd's material approval |
| Passenger Ferries | 5083 structural, 5052 secondary | Custom structural sections, safety rail profiles | Anodizing plus powder coating | ABS/Lloyd's; SOLAS compliance |
| Military Patrol | 5083-H116 or H321 | Blast-resistant designs, extruded aluminum airfoil | Hard anodizing, specialized coatings | MIL-SPEC; full material traceability |
| High-Performance Racing | 5083 hull, 6061-T6 framing | Airfoil sections, lightweight custom profiles | Lightweight anodizing or raw finish | Class rules (varies by racing organization) |
Notice how commercial vessels balance durability against cost? A fishing boat operator needs extrusions that survive 20 years of hard use, but excessive specifications eat into operating margins. The sweet spot typically involves 5083 alloy for structural components with hard anodizing rather than premium PVDF coatings - achieving excellent longevity without maximum expense.
Military applications accept no such compromises. The 5083-H116 and H321 temper designations indicate specific processing that maximizes resistance to stress corrosion cracking - essential when vessels may sit loaded in tropical harbors or experience rapid temperature cycling. Full material traceability means every extrusion links back to its original billet, heat treatment records, and quality inspection results.
Dimensional tolerances tighten considerably for commercial and military work. While recreational builds accept ±0.030-inch variations, certified commercial extrusions typically hold ±0.012 inches on critical dimensions. Military specifications often require ±0.008 inches or better, with 100% inspection documentation.
For specialty watercraft - racing boats, research vessels, or custom superyacht tenders - specifications blend elements from multiple categories. A racing hull might use 5083 for impact resistance while incorporating custom extruded aluminum airfoil sections for hydrofoil components, requiring tight tolerances on aerodynamic surfaces but allowing standard tolerances elsewhere.
Understanding these vessel-specific requirements positions you to specify appropriate extrusions - but the aluminum itself is only part of the equation. Surface treatments applied to your extrusions dramatically affect both longevity and appearance in marine environments.
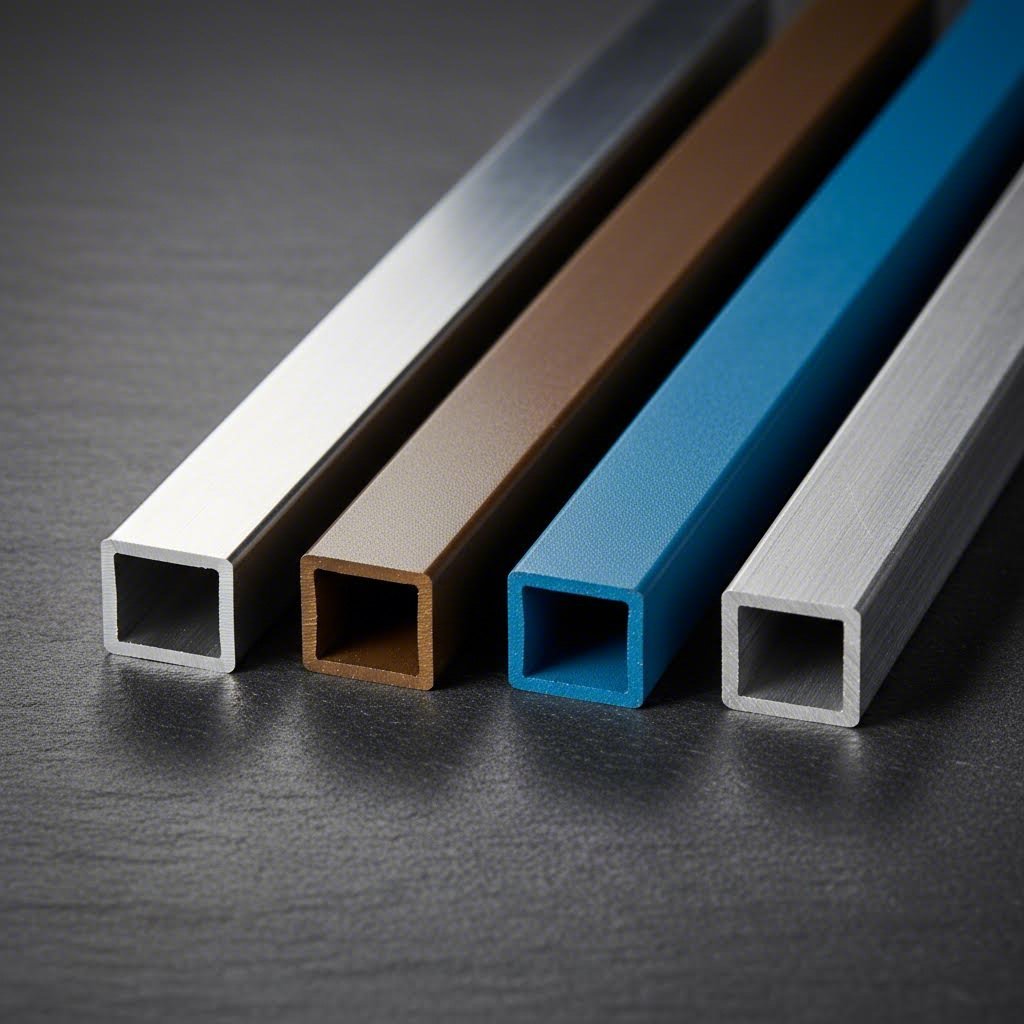
Your aluminum extrusions arrive with excellent natural corrosion resistance - but why stop there? Surface treatments transform good marine performance into exceptional longevity, reducing maintenance demands while opening up aesthetic possibilities that raw aluminum simply can't match.
Think of surface treatments as armor for your extrusions. The right coating protects against saltwater attack, UV degradation, and physical abrasion while potentially adding color, texture, or specialized properties. Whether you're finishing boat moulding trim on a weekend cruiser or protecting structural components on a commercial vessel, understanding your treatment options helps you balance protection, appearance, and budget.
Anodizing doesn't coat aluminum - it transforms the surface itself. This electrochemical process converts the outer layer of aluminum into aluminum oxide, creating an integral barrier that's actually part of the metal rather than an applied coating that might peel or chip.
Here's how it works: your extrusion becomes the anode in an electrolytic bath, typically containing sulfuric acid. When electrical current passes through, oxygen atoms bond with aluminum atoms at the surface, building up a dense oxide layer far thicker than aluminum's natural oxidation. Standard anodizing produces layers 0.0002 to 0.001 inches thick; hard anodizing pushes this to 0.002 inches or more.
Why does this matter for marine applications? The anodized layer resists saltwater penetration, shrugs off abrasion that would scratch raw aluminum, and accepts dyes for color customization. Unlike paint or powder coating, you can't accidentally scratch through to bare metal - the protection extends into the surface itself.
Anodizing options for marine extrusions include:
One consideration: anodizing works best on certain alloys. The 6XXX series produces consistent, attractive results ideal for visible applications. The 5XXX series can be anodized but may show slight color variations - acceptable for structural components but potentially problematic for decorative trim requiring uniform appearance.
When color options and UV protection take priority, powder coating delivers what anodizing cannot. This process applies dry powder electrostatically to your extrusions, then cures it in an oven where the particles melt and fuse into a continuous film. The result? A tough, attractive finish available in virtually any color imaginable.
Marine-grade powder coatings typically use polyester or polyester-epoxy hybrid formulations engineered to resist saltwater, UV exposure, and temperature cycling. Quality marine coatings maintain adhesion and color stability for 10-15 years in harsh coastal environments - far outperforming conventional paints.
For motorhome mouldings, aluminum trim for rv applications, and recreational vessel trim, powder coating offers an excellent balance of protection, aesthetics, and cost. The extensive color palette allows you to match or complement gel coat colors, create accent details, or achieve custom branding for commercial vessels.
Beyond standard powder coating, advanced finish options address extreme requirements:
How do these treatments compare for typical marine applications? Consider the following breakdown:
| Treatment Type | Corrosion Protection | UV Resistance | Color Options | Best Applications |
|---|---|---|---|---|
| Clear Anodizing | Very Good | Good | Natural silver only | Structural components, hidden elements |
| Colored Anodizing | Very Good | Good | Limited palette | Visible hardware, decorative trim |
| Hard Anodizing | Excellent | Good | Gray/black tones | Rub rails, high-wear surfaces |
| Powder Coating | Good to Very Good | Excellent | Unlimited | Visible trim, color-matched components |
| PVDF Coating | Excellent | Exceptional | Extensive | Commercial vessels, long-service applications |
| Micro-Arc Oxidation | Exceptional | Excellent | Limited | Military, extreme-duty components |
Surface treatment selection directly impacts maintenance requirements and service life. Properly anodized extrusions need only periodic washing to maintain appearance - no repainting, no rust treatment, no ongoing corrosion battles. Quality powder coating similarly reduces maintenance to simple cleaning, freeing you to enjoy your vessel rather than constantly protecting it.
For recreational builders, the choice often comes down to anodizing for components where natural aluminum appearance works, and powder coating where color matching or specific aesthetics matter. Commercial operators typically invest in harder anodizing or PVDF coatings, recognizing that higher initial treatment costs pay dividends through reduced maintenance and extended service life.
Whatever treatment you select, proper surface preparation before treatment proves critical. Clean, properly pretreated extrusions accept coatings uniformly and maintain adhesion throughout their service life. This preparation requirement connects directly to broader fabrication considerations - the practices you follow when cutting, welding, and installing your extrusions.
You've sourced the right alloys, selected appropriate profiles, and specified surface treatments - but here's where many projects stumble. The gap between receiving extrusions and successfully installing them trips up builders who overlook critical fabrication details. How you cut, weld, fasten, and prepare your aluminum directly determines whether your vessel performs flawlessly or develops problems within its first season.
Let's bridge that gap with practical guidance covering the fabrication techniques that preserve your extrusions' marine performance.
Welding aluminum differs fundamentally from steel welding. The metal's high thermal conductivity, oxide layer, and lower melting point demand specific techniques and equipment. Get it wrong, and you'll face porosity, cracking, or heat-affected zones that compromise corrosion resistance.
Two processes dominate marine aluminum welding: TIG (GTAW) and MIG (GMAW). Each suits different applications:
Alloy selection affects your welding approach significantly. The 5XXX series alloys weld readily without post-weld treatment - one reason they dominate structural marine applications. Simply use matching 5356 filler wire and maintain proper shielding gas coverage.
The 6XXX series presents more challenges. Welding heat softens the heat-affected zone, potentially reducing strength by 30-40% compared to the parent material. For structural 6061-T6 applications, you may need to account for this reduced strength in your design or specify post-weld heat treatment to restore properties.
Regardless of process, proper shielding gas proves essential. Pure argon works for most marine aluminum welding, though argon-helium mixtures improve penetration on thicker sections. Maintain gas flow rates between 25-40 CFH and use a gas lens to ensure consistent coverage.
Not every joint requires welding. Mechanical fasteners offer advantages in certain situations: easier disassembly for repairs, no heat-affected zones, and simpler installation for DIY builders lacking welding equipment. However, fastening aluminum correctly requires attention to galvanic corrosion prevention boats often overlook.
When selecting fasteners for marine aluminum, material compatibility matters enormously. Stainless steel fasteners (316 grade for saltwater) work well when properly isolated from aluminum. Aluminum fasteners eliminate galvanic concerns but offer lower strength. Monel fasteners provide excellent corrosion resistance but come at premium cost.
Preventing galvanic corrosion at fastener locations requires physical separation between dissimilar metals:
Before any joining operation - welding or fastening - proper surface preparation ensures lasting results. Follow this sequence for optimal outcomes:
Cutting and drilling aluminum extrusions requires similar attention. Use sharp carbide-tipped blades designed for non-ferrous metals - dull tooling generates excessive heat and produces rough edges that trap moisture. Lubricants improve cut quality and tool life; specialized aluminum cutting fluids work best, though even WD-40 outperforms dry cutting.
When bending extrusions, consider wall thickness and bend radius carefully. Thin-wall profiles bend readily but may buckle on tight radii. Heavy-wall sections resist buckling but require substantial force and may crack if bent too sharply. As a general rule, minimum bend radius should equal 1.5 to 3 times the wall thickness, depending on alloy and temper. The 6063-T5 temper bends more easily than 6061-T6; if your design requires sharp bends, specify accordingly.
These fabrication fundamentals apply whether you're building a single recreational boat or producing commercial vessels. However, the scale of your project significantly influences other considerations - particularly how you source materials and manage supplier relationships.
You've mastered alloy selection, profile matching, and fabrication techniques - but here's where many boat builders feel abandoned. Most aluminum extrusion content focuses on large shipbuilders ordering container loads of material. What about the weekend builder constructing a single skiff? Or the small shop producing a dozen boats annually? Understanding boat building material sourcing at every scale helps you navigate pricing structures, lead times, and supplier relationships that directly impact your project's success.
Whether you're ordering 50 feet of standard angle or developing custom profiles for a production run, knowing what drives costs empowers smarter purchasing decisions.
The cost difference between standard and custom aluminum extrusions often surprises first-time buyers. Standard profiles - those common shapes manufacturers keep in regular production - offer significant advantages for budget-conscious projects. You're sharing die costs across thousands of customers, benefiting from optimized production runs, and avoiding tooling investments entirely.
Custom profiles change the equation dramatically. When standard shapes won't meet your design requirements, you'll encounter die development costs that can range from $500 for simple solid shapes to $5,000 or more for complex hollow profiles. According to industry sources, hollow dies take several different forms including bridge, porthole, and spider designs - each with distinct advantages, disadvantages, and cost implications.
Here's how custom aluminum extrusion cost breaks down:
For small boat builders, this math often points toward adapting designs to use standard profiles wherever possible. Reserve custom extrusions for components where off-the-shelf shapes truly won't work - perhaps a specialized rub rail profile or integrated mounting channel. Every component that uses standard shapes reduces your tooling investment and simplifies future replacement part sourcing.
Minimum order quantities represent another critical cost factor. As aluminum extrusion specialists explain, MOQs exist for sound economic and technical reasons: die preparation overhead, press setup time, and quality verification all add fixed costs that must be distributed across production volume.
Typical MOQs vary by profile complexity and supplier capability:
Small builders feeling squeezed by MOQs have options. Some suppliers offer "sample runs" at premium pricing to help evaluate new profiles before committing to production quantities. Others maintain relationships with distributors who aggregate demand from multiple small buyers. And increasingly, online marketplaces connect builders needing small quantities with suppliers willing to accommodate them.
Marine aluminum supplier selection extends beyond finding the lowest price. The wrong supplier delivers late, ships inconsistent quality, or disappears when you need technical support. Thorough evaluation prevents these headaches - and the guidance applies whether you're sourcing domestically or internationally.
When evaluating any potential supplier, assess these critical capabilities:
Lead times deserve careful attention during marine aluminum supplier selection. Three phases determine your total wait time:
Tooling Lead Time: For custom profiles, die manufacturing typically requires 2-4 weeks. Complex shapes or tight tolerances extend this timeline. Standard profiles eliminate this phase entirely.
Extrusion Lead Time: Production scheduling varies by supplier workload. Expect 2-4 weeks for standard orders, though some suppliers offer expedited processing. As industry experts note, the die must be tested to ensure extrusions match specifications before production begins.
Fabrication Lead Time: If your order includes cutting, drilling, machining, or surface treatment, add additional time. Complex secondary operations can extend total lead time by days or weeks depending on requirements.
For budget planning across different project scales, consider these guidelines:
Don't overlook additional costs beyond base material pricing. Packaging for shipping, freight charges, customs duties for international orders, and payment terms all affect total project cost. Request complete quotes specifying all charges before committing to suppliers.
Finally, verify supplier reliability through references. Ask for customer references or case studies, particularly from marine applications. A supplier excelling in architectural extrusions may lack experience with marine alloy specifications or certification requirements. Direct feedback from similar buyers reveals real-world performance that sales presentations won't capture.
Armed with sourcing knowledge and budget clarity, you're positioned to select not just materials but the right manufacturing partner - a decision that influences everything from initial quotes through long-term support.
You've navigated alloy selection, profile matching, surface treatments, and fabrication techniques - now comes the decision that ties everything together. The aluminum extrusion manufacturer marine builders choose determines whether carefully planned specifications translate into quality components or become sources of frustration. A capable partner does more than ship metal; they provide technical guidance, solve production challenges, and deliver consistent quality that keeps your project on schedule.
Think of this relationship as a collaboration rather than a transaction. The right supplier understands marine requirements, anticipates potential issues, and offers solutions before problems derail your timeline. How do you identify such a partner? Let's examine the capabilities that separate exceptional custom boat extrusion services from basic commodity suppliers.
Not all extrusion suppliers can serve marine applications effectively. The combination of alloy expertise, equipment range, and finishing capabilities required for boat building narrows the field considerably. When evaluating potential partners, prioritize these critical factors:
Technical communication reveals a supplier's true capability level. As industry guidance emphasizes, a well-chosen extrusion partner is more than just a vendor - they are a key contributor to your success. Professional suppliers offer Design for Manufacturability (DFM) feedback, suggest cost optimization alternatives, and proactively identify potential issues before production begins.
The most critical factor in aluminum extrusion partner selection? Matching supplier capabilities to your specific project requirements. A supplier excelling in architectural applications may lack marine alloy expertise, while one focused on automotive work might not offer the surface treatments your vessel demands. Evaluate each candidate against your actual needs - not their most impressive capabilities.
Ready to move from planning to production? The path from concept to delivered extrusions follows predictable steps when you're working with an experienced partner.
Begin by preparing clear documentation of your requirements. Detailed drawings showing cross-sectional dimensions, length requirements, alloy specifications, and surface finish expectations give suppliers the information needed for accurate quoting. Include tolerance requirements and identify critical dimensions versus those with more flexibility.
Request samples before committing to production quantities. Reputable suppliers provide sample sections - sometimes at nominal cost - allowing you to verify fit, finish, and quality before investing in full production runs. This small upfront investment prevents costly surprises.
Discuss certification requirements early. If your vessel requires ABS classification or other third-party approval, your supplier needs to understand documentation requirements from the start. Adding certification requirements after production begins creates delays and additional costs.
For builders seeking comprehensive capability under one roof, manufacturers offering end-to-end services simplify project management considerably. Shengxin Aluminium exemplifies this integrated approach, combining over 30 years of extrusion experience with extensive processing capabilities. Their facility operates 35 extrusion presses ranging from 600T to 5500T - covering everything from delicate trim profiles to heavy structural sections.
Beyond extrusion, Shengxin provides the secondary operations marine builders need: CNC machining centers handle precise cutting, drilling, and bending to specification. Their surface treatment capabilities include anodizing in custom colors, powder coating, PVDF coatings for extreme durability, and micro-arc oxidation for applications demanding maximum hardness and corrosion resistance.
This integration matters because it eliminates coordination headaches. Rather than managing separate suppliers for extrusion, machining, and finishing - each with their own lead times, quality standards, and communication requirements - you work with a single technical team from die development through mass production. For builders exploring custom extrusion and deep processing services, this approach offers both convenience and quality consistency.
Whatever partner you choose, establish clear communication expectations from the start. Regular project updates, responsive technical support, and transparent handling of any issues distinguish professional relationships from transactional ones. Your extrusion partner should feel invested in your project's success - because ultimately, their reputation depends on your satisfaction.
The journey from aluminum billet to finished marine component involves countless decisions. By matching alloys to applications, profiles to components, surface treatments to environments, and capabilities to requirements, you've positioned yourself to source extrusions that perform flawlessly throughout your vessel's service life. The right partner transforms these decisions into delivered quality - completing the chain from specification to installation.
Marine aluminum extrusions primarily use two alloy families: 5XXX series (5052, 5083, 5086) and 6XXX series (6061-T6, 6063). The 5XXX series offers exceptional corrosion resistance ideal for saltwater hull applications, with 5083 delivering the highest strength for military and commercial vessels. The 6XXX series provides superior surface finish and easier machinability, making it perfect for decorative trim and above-waterline components. Freshwater boats can use 6061-T6 for structural elements, while saltwater vessels should specify 5XXX alloys for any direct water contact.
Marine aluminum extrusions can receive several protective treatments: clear or colored anodizing creates an integral oxide layer for corrosion resistance; hard anodizing (Type III) provides superior wear resistance for rub rails; powder coating offers unlimited color options with excellent UV protection; PVDF coatings deliver exceptional chemical resistance for commercial vessels; and micro-arc oxidation creates ceramic-like surfaces for extreme-duty military applications. Manufacturers like Shengxin Aluminium offer comprehensive surface treatment capabilities including custom anodizing colors and multi-layer coating systems.
Standard profiles offer lower costs and faster availability since you share die expenses across thousands of customers. Custom extrusions require die development costing $500-$5,000+ depending on complexity, plus minimum order quantities typically starting at 300-500 pounds. For small boat builders, adapting designs to use standard profiles wherever possible reduces tooling investment. Reserve custom profiles for components where off-the-shelf shapes truly won't work, such as specialized rub rails or integrated mounting channels.
Quality marine aluminum suppliers should demonstrate ISO 9001 certification for systematic quality management. For commercial vessels, look for familiarity with ASTM B221 (aluminum extrusion specifications), American Bureau of Shipping (ABS) material approval, or Lloyd's Register classification. Military applications require MIL-SPEC compliance with full material traceability. Suppliers should provide mill test reports, dimensional inspection records, and certification documentation upon request.
TIG welding delivers cleaner, more precise welds ideal for thin-wall extrusions under 3/16-inch and visible joints requiring aesthetic finish. It offers complete control over heat input but requires more skill and slower travel speeds. MIG welding provides faster deposition rates and easier learning curve, best suited for heavier structural sections and production welding. For 5XXX series alloys, use matching 5356 filler wire. Note that 6XXX series may require post-weld heat treatment to restore strength in heat-affected zones.


 dịch vụ trực tuyến
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Việt
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Українська