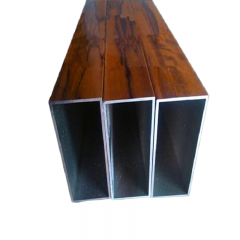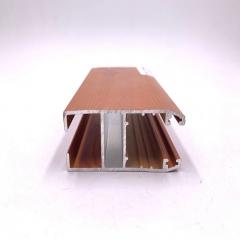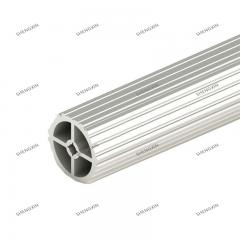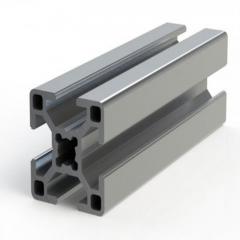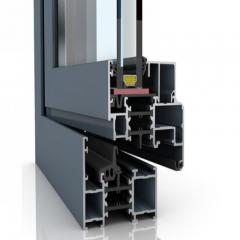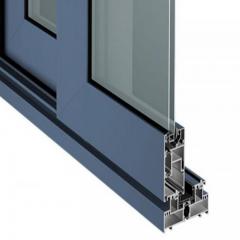
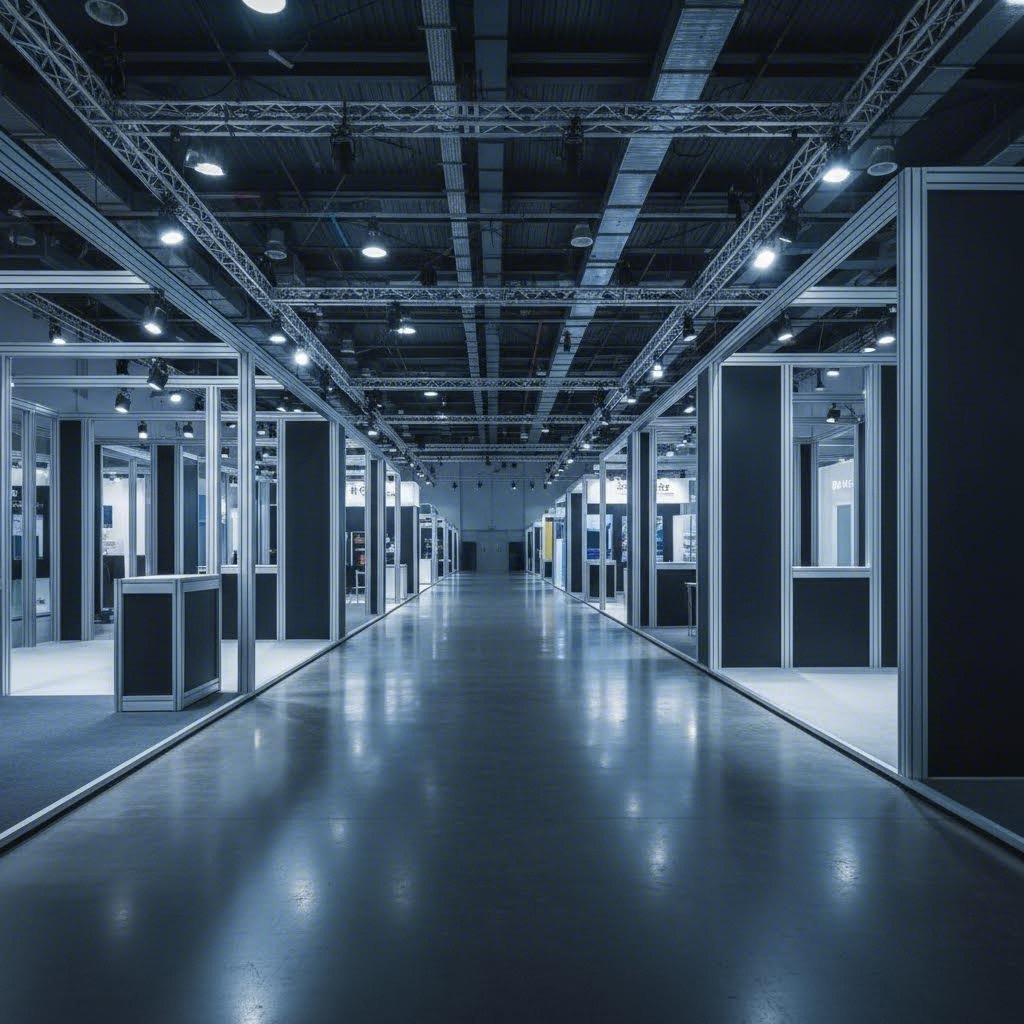
Walk into any major trade show today, and you'll notice something striking: the sleek, seamlessly constructed booth structures that seem to appear almost overnight. Behind these impressive displays lies a manufacturing marvel that has revolutionized the exhibit industry—aluminum extrusions. These versatile building components have become so fundamental to modern exhibit design that imagining a trade show floor without them feels almost impossible.
But what exactly are these components, and why has the industry embraced them so completely? Let's break it down in terms anyone can understand.
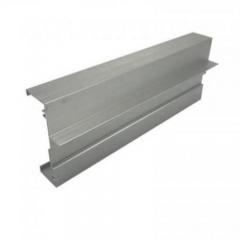
Picture this: heated aluminum, brought to temperatures between 750 and 900 degrees Fahrenheit, is forced through a specially shaped opening called a die. What emerges from the other side? A continuous length of aluminum with a perfectly consistent cross-sectional shape—whether that's a simple tube, a complex T-slot channel, or an intricate profile designed for specific connection purposes. This process, known as aluminum extrusion, creates the fundamental building blocks that exhibit designers rely on daily.
Think of it like a sophisticated Play-Doh factory. Just as children push soft clay through shaped openings to create fun forms, industrial presses force malleable aluminum through precision-engineered dies. The result is remarkably consistent: each piece of aluminum extrusion emerges with identical dimensions, ready to connect seamlessly with its counterparts.
As Norm Friedrich, president and CEO of Octanorm, explains: "As an engineer, it's the mechanical properties of extruded aluminum that continue to amaze me. Based on the weight to strength ratio, there is no other material that compares."
Imagine an adult-sized Erector Set—that's essentially what modern aluminum extrusion systems offer exhibit designers. Each extrusion frame component is engineered to connect with others in predictable, reliable ways. Corner pieces snap together with wall sections. Vertical posts accept horizontal beams. The entire system works like building blocks, enabling exhibitors to construct everything from simple 10x10 booths to elaborate multi-story installations.
This modular approach represents a dramatic departure from traditional exhibit construction. Before 1968, when Hans Staeger introduced the first extruded exhibition stand system at EuroShop in Düsseldorf, most exhibits were heavy wooden structures requiring skilled carpenters and specialized tools for every setup. Today, a single installer can often handle an entire aluminum extrusion case of components, assembling a complete booth in a fraction of the time.
Why has this shift been so complete? Consider the key advantages:
Modern systems have evolved far beyond the early "cookie cutter" designs that once limited creativity. Today's aluminum extrusions virtually disappear behind graphics and finishes, allowing exhibitors to achieve truly custom looks. Whether you're showcasing products in a glass showcase or creating an interactive glass show case display, the underlying aluminum framework provides the invisible structural integrity that makes it all possible.
In the sections ahead, we'll explore everything from alloy selection to surface treatments, component types to logistics planning—giving you the comprehensive knowledge needed to make informed decisions about aluminum extrusions for your exhibit structures. Whether you're a first-time exhibitor or a seasoned trade show veteran looking to optimize your approach, this guide will take you from the fundamentals to show-floor success.
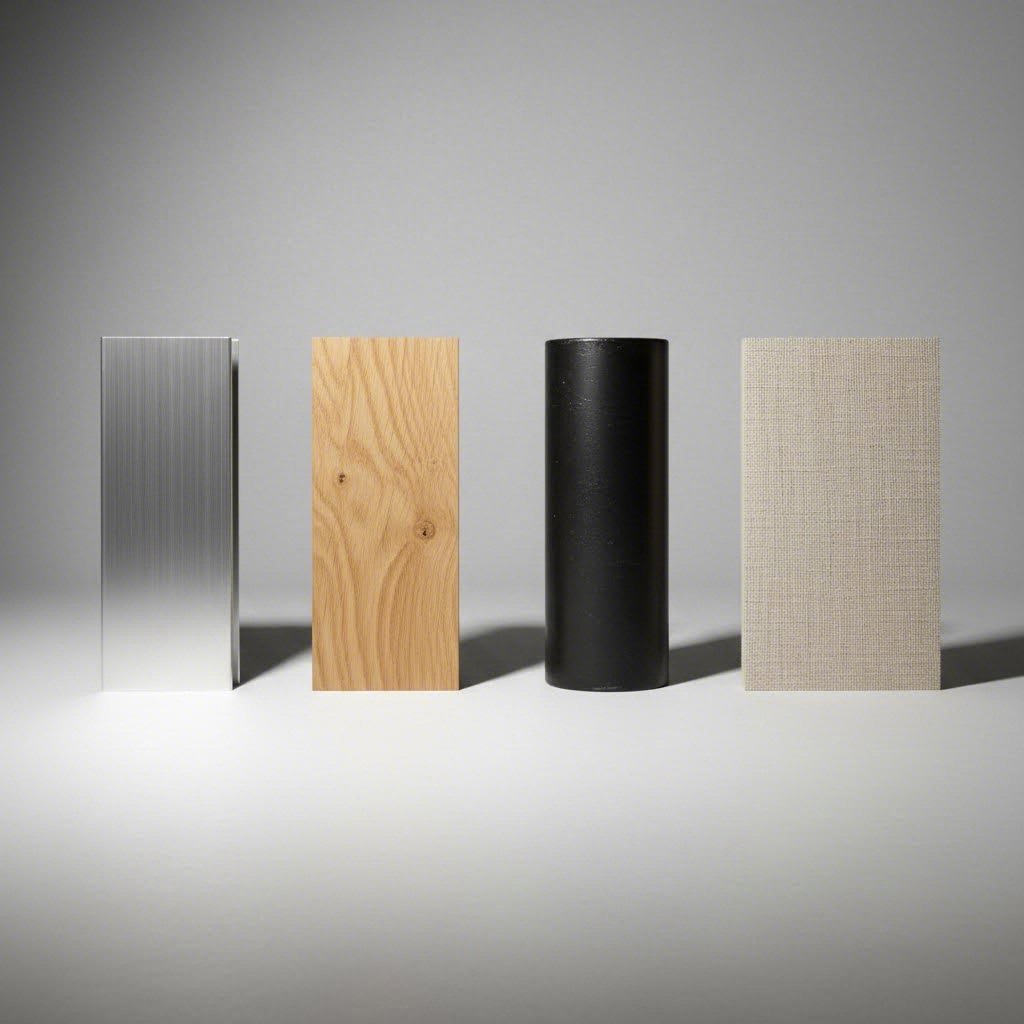
So you're evaluating materials for your next exhibit structure. Maybe you've heard aluminum is the industry standard, but you're wondering: is it really worth it? Could traditional wood offer that premium look you're after? What about the affordability of fabric systems? Let's cut through the noise and examine exactly how aluminum frame extrusions stack up against every major alternative—using real performance criteria that matter on the show floor.
Here's a scenario every exhibitor dreads: your shipping costs just doubled because your booth materials pushed you into a higher freight bracket. Weight isn't just about muscle strain during setup—it directly impacts your bottom line through shipping fees, drayage charges, and labor costs.
Aluminum's strength-to-weight ratio is where the material truly shines. As industry experts note, "based on the weight to strength ratio, there is no other material that compares." This isn't marketing speak—it's engineering reality. Aluminum delivers structural integrity at roughly one-third the weight of steel, meaning your extruded aluminum housing for displays and enclosures can support substantial loads while remaining remarkably easy to transport.
Consider this practical comparison: aluminum extrusion furniture and display structures require significantly fewer handlers during load-in and load-out. When you're racing against setup deadlines with union labor on the clock, that efficiency translates directly into cost savings.
Trade show life is brutal on materials. Your exhibit gets packed, shipped across the country, assembled by different crews, disassembled, and repeated dozens of times per year. Which materials actually survive this punishment?
Aluminum's natural corrosion resistance gives it a decisive edge. Unlike steel, which requires constant vigilance against rust, or wood, which warps and deteriorates when exposed to humidity swings between climate-controlled warehouses and outdoor loading docks, aluminum maintains its structural properties show after show. The material handles extreme temperature variations without expanding, contracting, or losing dimensional accuracy.
Fabric systems, while lightweight, face different durability challenges. Graphics fade, materials stretch, and the "fresh" appearance diminishes with each use. Extruded aluminum enclosures and frames, by contrast, can serve as the foundation for countless graphic updates—your framework becomes a long-term investment that outlasts multiple branding refreshes.
Smart exhibitors think beyond the initial purchase price. When you factor in reusability, maintenance, shipping, storage, and setup labor, the cost picture shifts dramatically.
| Criteria | Aluminum Extrusions | Wood Construction | Steel Frames | Fabric Systems |
|---|---|---|---|---|
| Weight | Lightweight (excellent strength-to-weight ratio) | Heavy (dense materials increase shipping) | Very Heavy (highest shipping costs) | Very Lightweight (lowest shipping costs) |
| Durability | Excellent (corrosion resistant, handles temperature extremes) | Moderate (susceptible to warping, humidity damage) | Good (but prone to rust without treatment) | Limited (fading, stretching over time) |
| Reusability | Excellent (decades of use, infinitely reconfigurable) | Limited (often single-use or few reuses) | Good (if properly maintained) | Moderate (graphics need frequent replacement) |
| Assembly Time | Fast (modular connections, minimal tools) | Slow (skilled labor required, complex construction) | Moderate (heavier handling, bolted connections) | Very Fast (tension systems, quick deployment) |
| Shipping Costs | Low to Moderate | High | Very High | Very Low |
| Aesthetic Flexibility | High (accepts any finish, disappears behind graphics) | High (premium natural look, fully customizable) | Moderate (industrial appearance, limited finishes) | High (vibrant graphics, modern look) |
Wood certainly delivers that premium, organic aesthetic that some luxury brands desire. As industry sources confirm, wood provides "an elegant, organic aesthetic that enhances your brand image" and remains "a superb option for exhibitors seeking an upmarket or environmentally conscious look." However, wood's weight and susceptibility to damage often make it impractical for exhibitors attending multiple shows annually.
Steel offers unmatched structural strength for heavy-duty applications—supporting large monitors, elaborate lighting rigs, or multi-story configurations. But the weight penalty is severe. Steel frames are "heavier than aluminium" and require "extra structural reinforcement," driving up both shipping and handling costs significantly.
Fabric systems win on initial cost and portability. They're "easy to transport and set up" and offer a "more affordable option" compared to rigid materials. However, their limited lifespan and reduced structural capabilities make them better suited for simple backdrops rather than complex exhibit structures.
When you examine item extruded aluminium components over a five-year horizon, the math becomes clear. An aluminum system that costs more upfront but survives 50+ shows without replacement delivers far better value than cheaper alternatives requiring frequent repairs or complete rebuilds. The versatility of aluminum—where the same components reconfigure for different booth sizes and layouts—compounds these savings dramatically.
Understanding why aluminum dominates modern exhibit construction is just the beginning. The next critical decision? Selecting the right aluminum alloy for your specific application—a choice that affects everything from structural performance to surface finish quality.
Here's something frustrating: you've decided aluminum extrusions are the right choice for your exhibit, but suddenly you're confronted with alloy numbers like 6063, 6061, and 6005. What do these numbers mean? Does it actually matter which one you choose? The short answer is yes—alloy selection directly impacts your exhibit's structural performance, surface finish quality, and long-term durability.
The good news? You don't need a materials science degree to make smart alloy decisions. Let's demystify the three primary alloys you'll encounter in the exhibit industry and help you match the right aluminum profile extrusions to your specific requirements.
If you've browsed any extruded aluminum shapes catalog for exhibit applications, you've likely seen 6063 listed repeatedly. There's a reason this alloy dominates the industry: it's specifically engineered for the extrusion process itself.
6063 aluminum is alloyed primarily with magnesium (0.45-0.9%) and silicon (0.2-0.6%), creating what engineers call the Al-Mg-Si system. This combination delivers something exhibit designers deeply value—exceptional surface finish quality. When your aluminum framework will be visible or requires anodizing in custom brand colors, 6063 responds beautifully to surface treatments.
Key properties that make 6063 ideal for standard exhibit applications:
For the vast majority of exhibit structures—wall panels, door frames, sign frames, and decorative trim—6063 delivers the perfect balance of workability and performance. It's no coincidence that industry experts identify 6063 as "the most popular extruded aluminum alloy for thin wall and architectural applications."
What happens when your exhibit needs to support substantial weight? Picture a large overhead sign, multiple flat-screen monitors, or elaborate lighting rigs suspended from your framework. This is where 6061 aluminum earns its place in your aluminum shapes catalog of options.
6061 is a precipitation-hardened alloy containing slightly different chemistry—notably adding copper (around 0.28%) to the magnesium-silicon base. This copper addition enhances grain structure and resulting strength after heat treatment, making 6061 the go-to choice when structural demands increase.
Key properties that distinguish 6061 for load-bearing exhibit applications:
Here's a practical rule of thumb: when material strength is the primary concern, 6061 is typically the better choice. As materials specialists note, "if strength is the determining factor for an application, 6061 may be the optimal choice." For exhibit structures requiring exceptional load-bearing capacity—multi-story installations, heavy media walls, or industrial product displays—6061 provides the necessary structural backbone.
Beyond the 6063/6061 decision, a third alloy deserves your attention: 6005 aluminum. This alloy occupies the middle ground, offering what industry sources describe as "a medium-strength structural extrusion alloy" that balances strength and formability.
6005 contains slightly higher silicon content (0.6-0.9%) than 6063 and can include up to 0.5% manganese. The result? Tensile strength around 310 MPa—matching 6061—while maintaining better extrudability than that stronger alloy. For modular exhibit structures requiring both good structural performance and reasonable manufacturing flexibility, 6005 offers a compelling middle path.
So how do you actually decide? Consider these practical questions:
Many professional exhibit systems actually combine alloys strategically. Visible trim and decorative elements might use 6063 for its beautiful finish, while structural uprights and load-bearing horizontal members utilize 6061 or 6005 for enhanced strength. This hybrid approach optimizes both aesthetics and performance.
Understanding alloy selection gives you a critical foundation, but aluminum profiles don't work alone. They connect, interlock, and combine through an ecosystem of specialized components—the hardware that transforms simple extruded aluminum sections into complete, functional exhibit structures.
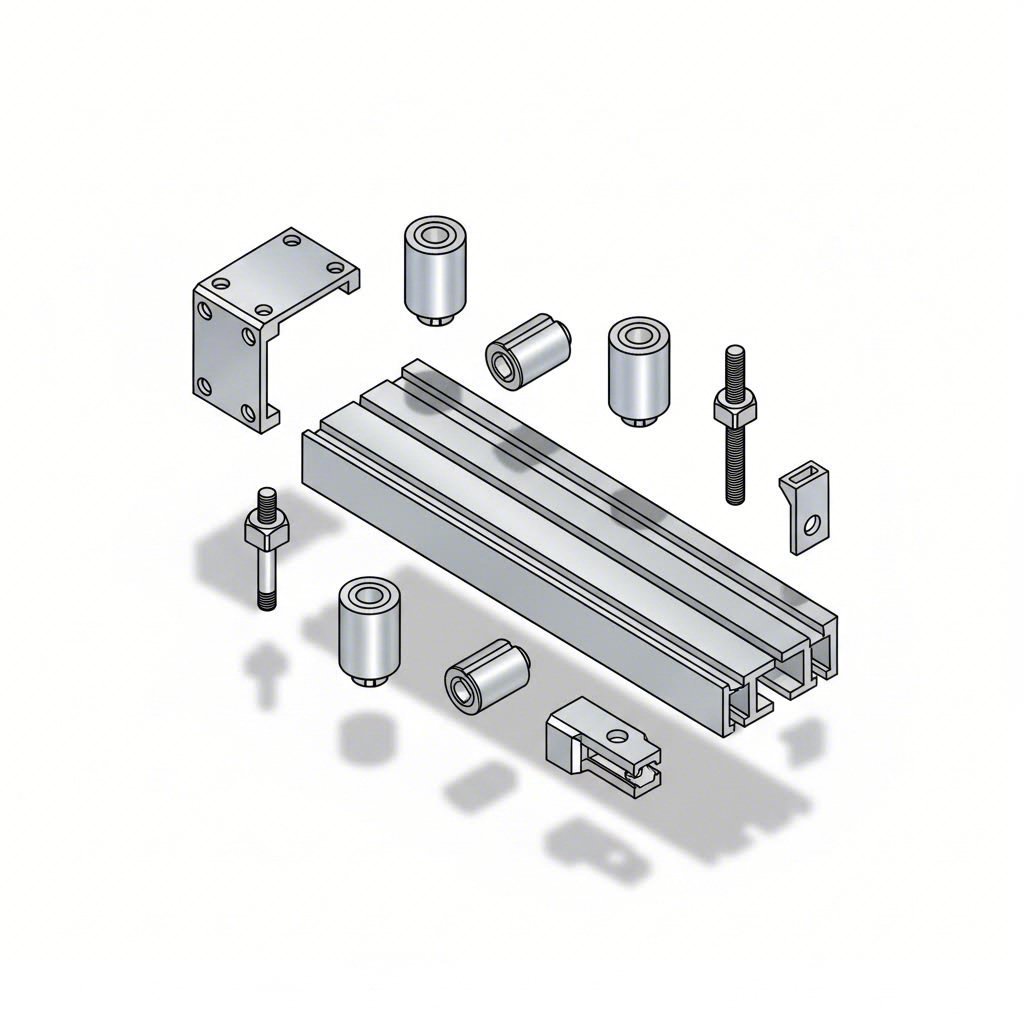
You've selected your aluminum alloy. You understand why extruded profiles outperform traditional materials. But here's the question that separates successful exhibit builders from frustrated ones: how do all these pieces actually connect? The answer lies in a carefully engineered ecosystem of components—each designed for specific functions that enable the modular magic trade show veterans rely on.
Think of it like this: aluminum profiles are the bones, but connectors, tracks, and trim pieces are the joints and finishing touches that bring your exhibit structure to life. Understanding each component's role transforms you from someone who assembles exhibits to someone who designs them strategically.
Every exhibit structure needs corners. Sounds obvious, right? But the way those corners connect determines everything from assembly speed to structural rigidity. Modern aluminum extrusion systems offer multiple connector options, each suited to different situations.
Standard corner brackets represent the workhorse of exhibit assembly. These L-shaped plates feature holes aligned with the T-slots on both connecting profiles, creating strong 90-degree joints. You'll find variations including:
For complex intersections where three or more profiles meet—imagine the corner of a cube-shaped display—specialized 8-way connectors simplify what would otherwise require multiple brackets. These cube connectors accept profiles from six directions simultaneously, enabling rapid assembly of three-dimensional frameworks without the clutter of overlapping hardware.
Hidden connectors offer another approach entirely. Rather than external brackets visible on the finished structure, these fasteners work inside the T-slots themselves. The result? Cleaner aesthetics that let your graphics and products take center stage. This matters especially when building an aluminum extrusion display case where every visible element should enhance rather than distract from your presentation.
The T-slot is the defining feature that makes aluminum extrusion systems so versatile. These precisely shaped channels running along profile lengths accept specialized T-nuts that can slide anywhere along the extrusion before being locked into position. It's this simple mechanism that enables the "building block" flexibility exhibit designers love.
T-slotted profiles come in various configurations:
The beauty of T-slot systems lies in their adjustability. Need to reposition a monitor mount? Loosen the bolts, slide the bracket to the new location, and retighten. Want to add shelving mid-show? Insert T-nuts and attach new components without disassembling existing structure. This flexibility proves invaluable when booth layouts must adapt to different show configurations.
Aluminum extrusion trim pieces work with T-slots to deliver finished appearances. These cover strips snap into the slots, concealing fastener heads and creating smooth, professional surfaces. Some exhibitors run wiring through the slots before covering them—keeping cables organized and invisible while maintaining easy access for future modifications.
Even miniature extrusions utilize T-slot principles at smaller scales, enabling detailed work on compact displays, product showcases, and point-of-purchase installations where full-size profiles would overwhelm the design.
Static exhibits are predictable. Dynamic exhibits capture attention. Aluminum track extrusion systems enable the movement that makes displays memorable—sliding panels, repositionable graphics, adjustable shelving, and interactive elements that engage visitors.
An extruded aluminium track typically features a specialized channel designed to accept rollers, slides, or guide wheels. Common applications include:
The aluminum extrusion slider components that work within these tracks are engineered for smooth, quiet operation—critical in trade show environments where ambient noise levels already challenge conversation. Quality track systems handle repeated cycling without developing the wobble or resistance that plagues inferior designs.
Panel extrusions serve a complementary function, providing channels specifically designed to grip graphic substrates, acrylic sheets, or composite panels. The aluminum track extrusion accepts the panel edge, holding it securely while allowing quick graphic swaps between shows or even during multi-day events.
Before ordering components for your next exhibit structure, verify you've accounted for every element that transforms raw profiles into a finished display:
These components work as an integrated system. The standardization across quality manufacturers means profiles, connectors, and accessories interface predictably—though mixing brands requires careful verification of dimensional compatibility, as even slight variations in slot geometry can cause frustrating fitment issues.
With your component knowledge in place, the next critical step involves translating these building blocks into actual booth configurations. How many profiles does a 10x10 booth really require? What about larger island installations? Understanding the planning methodology for different booth sizes ensures you order exactly what you need—nothing more, nothing less.
Here's where theory meets reality. You understand aluminum alloys, you know your components—but how many extrusions do you actually need for your booth? Surprisingly, this practical question remains unanswered across most industry resources. Let's fix that with a systematic planning framework that scales from compact inline booths to expansive island configurations.
Before calculating quantities, you need to understand the rules governing your space. Trade show venues enforce strict height and construction guidelines that directly impact your aluminum extrusion panels and structural framework requirements.
The standard 10x10 inline booth—100 square feet of exhibiting space—represents the entry point for most trade show participants. Despite its compact footprint, this configuration requires thoughtful planning to maximize impact while respecting venue regulations.
According to industry booth design regulations, inline 10x10 booths face specific constraints:
These restrictions shape your aluminum extrusion bar and profile requirements significantly. For a basic 10x10 backwall-focused design, you'll typically need:
The planning methodology starts with your design concept. Sketch your booth layout, identify every vertical and horizontal element, then measure each required length. Add 10-15% contingency for cutting waste and potential modifications during setup.
Island booths—exposed to aisles on all four sides—offer maximum visibility but demand more sophisticated structural planning. The minimum size for island configurations is typically 20x20 feet, with regulations permitting significantly greater height allowances.
The height advantages for larger booth types create new possibilities:
| Booth Type | Minimum Size | Maximum Height | Hanging Signs Permitted | Tower Maximum Height |
|---|---|---|---|---|
| Standard Inline (10x10, 10x20) | 100 sq ft | 8 feet (back wall) | No | N/A |
| Perimeter Inline | 100 sq ft | 12 feet (back wall) | No | N/A |
| Standard Peninsula | 20x20 ft | 8 feet (center 10 ft); 4 feet (sides) | Yes | 8 feet |
| Split Island Peninsula | 20x20 ft | 12 feet | Yes | 12 feet |
| Island | 20x20 ft | 16 feet (12 feet recommended) | Yes | 16 feet |
For a 20x20 island booth, your aluminum panel extrusions and structural components multiply accordingly. A typical configuration might require:
Larger custom footprints—30x30, 40x40, or irregular configurations—follow the same planning principles but require engineering review for structural integrity, especially when incorporating multi-story elements or heavy suspended components.
Modern exhibits increasingly feature suspended elements: large-format signage, multiple monitors, theatrical lighting rigs, and even product displays hanging from overhead frameworks. These applications demand careful attention to load-bearing capacity—and directly influence which aluminum extrusion panels and profiles you specify.
Consider these structural factors when planning overhead elements:
For hanging signage applications, aluminum sign frame extrusions specifically engineered for overhead mounting provide integrated attachment points and verified load ratings. Generic structural profiles can work but require careful calculation to ensure adequate safety margins.
A practical approach to load planning:
Height restrictions also affect extrusion selection beyond simple length requirements. Taller structures experience greater lateral forces, requiring either heavier-gauge profiles or additional cross-bracing to prevent sway. As one industry planning guide emphasizes, exhibitors should begin design work 8-12 weeks before show dates to allow proper engineering review for complex configurations.
Smart exhibitors also plan for the realities of trade show timelines. Setup windows are notoriously tight—often just hours to transform empty floor space into a complete branded environment. Your aluminum extrusion bar quantities should account for modular assembly approaches that enable rapid construction without specialized tools or extensive labor crews.
With your structural framework planned and component quantities calculated, the next consideration transforms functional aluminum into brand-aligned visual impact: surface treatments and finishing options that elevate your exhibit from industrial framework to polished brand showcase.
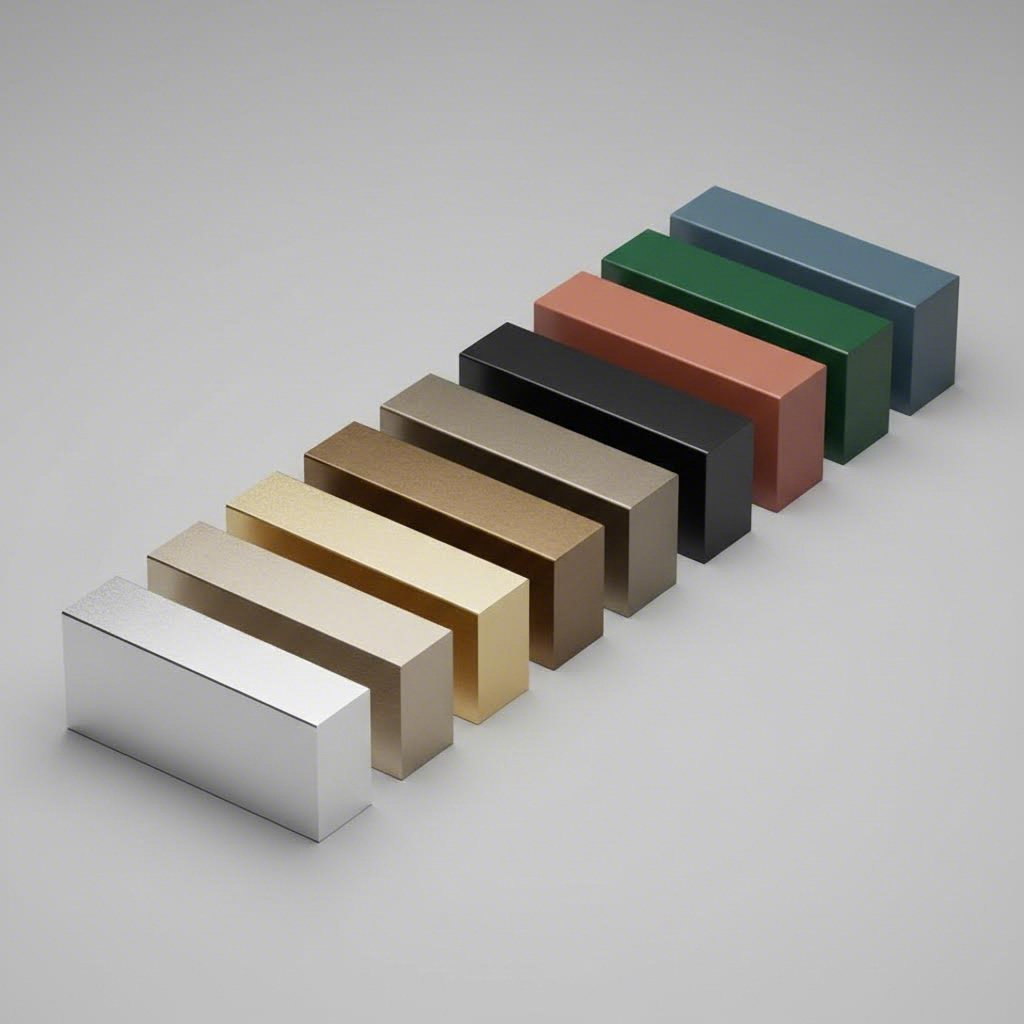
Your aluminum framework is engineered, your components selected, and your booth dimensions mapped. But here's the reality: raw aluminum doesn't exactly scream "premium brand experience." The silver-gray metal fresh from extrusion needs transformation—surface treatments that deliver both visual impact and long-term durability across countless shows.
Surface finishing isn't merely cosmetic. The treatment you choose affects how your exhibit handles scratches during transport, resists fingerprints from curious attendees, and maintains its appearance after years of setup and teardown cycles. Let's explore the finishing options that turn functional aluminium extrusion trim and structural components into polished brand showcases.
Anodizing remains the most popular surface treatment for aluminum extrusions in exhibit applications—and for good reason. This electrochemical process creates an integral oxide layer that becomes part of the aluminum itself rather than sitting on top as a coating.
Imagine dipping your aluminum profile into an acid bath while running electrical current through it. The result? A controlled oxidation that produces a surface dramatically harder than raw aluminum. This anodized layer resists scratches, won't peel or flake like paint, and accepts dyes that penetrate into the oxide structure for permanent coloration.
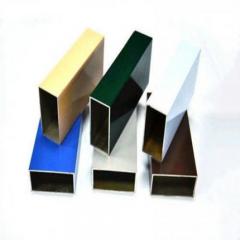
Standard anodizing colors available from quality manufacturers include:
What makes anodizing particularly valuable for exhibit structures? The durability factor. According to industry specialists, anodized aluminum extrusions possess "higher level of strength" with "capability to be protected from harsh environments." Your aluminium extrusion box structures and visible framework elements maintain their appearance show after show.
Custom color anodizing opens additional possibilities for brand-specific finishes. When standard catalog colors don't match your corporate palette, manufacturers with advanced anodizing capabilities can develop proprietary colors that align precisely with your brand guidelines.
When exact brand color matching matters—and it usually does—powder coating delivers what anodizing cannot: virtually unlimited color options with consistent results.
The powder coating process applies electrostatically charged dry powder to the aluminum surface, then cures it in an oven where the particles fuse into a smooth, durable film. Unlike liquid paints, powder coating produces no volatile organic compounds (VOCs) and creates a thicker, more impact-resistant finish.
Benefits of powder coating for aluminum window extrusions and exhibit structures include:
The practical implications for exhibitors? You can specify window extrusion profiles and structural components in exactly your brand's signature blue, red, or any custom shade—maintaining visual consistency across all marketing touchpoints.
One consideration: powder coating sits atop the aluminum rather than integrating with it like anodizing. For high-wear areas subject to repeated contact, specify appropriate coating thickness and consider touchup kits for field repairs.
Beyond standard anodizing and powder coating, specialty finishes address specific performance requirements and aesthetic goals that standard treatments can't achieve.
PVDF Coatings for Outdoor Exhibits
Taking your exhibit outdoors—festival booths, outdoor trade shows, permanent installations? PVDF (polyvinylidene fluoride) coatings deliver the weathering resistance that standard finishes can't match.
PVDF coatings, including premium formulations like Kynar, contain over 70% fluorocarbon resin that creates exceptional barriers against UV degradation, chemical exposure, and environmental pollution. According to coating performance data, PVDF-treated surfaces maintain color and gloss "for over 30 years, even in harsh climates" with temperature resistance spanning -60°C to 150°C.
Key PVDF performance characteristics:
For aluminum window extrusion profiles used in permanent outdoor installations or exhibits traveling to harsh environments, PVDF represents the premium protection choice despite higher initial cost.
Mechanical Polishing and Brushing
When you want aluminum to look like aluminum—but better—mechanical finishing creates refined surfaces impossible through chemical treatment alone. Polished aluminum achieves mirror-like reflectivity, while brushed finishes produce sophisticated satin textures with directional grain patterns.
Micro-Arc Oxidation
This advanced plasma electrolytic process creates ceramic-like oxide coatings significantly harder than standard anodizing. For exhibit components subject to extreme wear—high-traffic flooring transitions, frequently adjusted mechanisms, or industrial demonstration displays—micro-arc oxidation provides exceptional abrasion resistance.
Here's the practical reality: coordinating separate suppliers for extrusion, machining, and finishing creates complexity, delays, and quality control challenges. Each handoff introduces potential for miscommunication, dimensional variation, and project timeline disruption.
Manufacturers with comprehensive in-house finishing capabilities streamline this entire process. When your extrusion supplier also handles anodizing in custom colors like champagne and rose gold, powder coating to your exact brand specifications, PVDF coating for outdoor applications, and specialty treatments like micro-arc oxidation, you gain single-source accountability from die development through finished components.
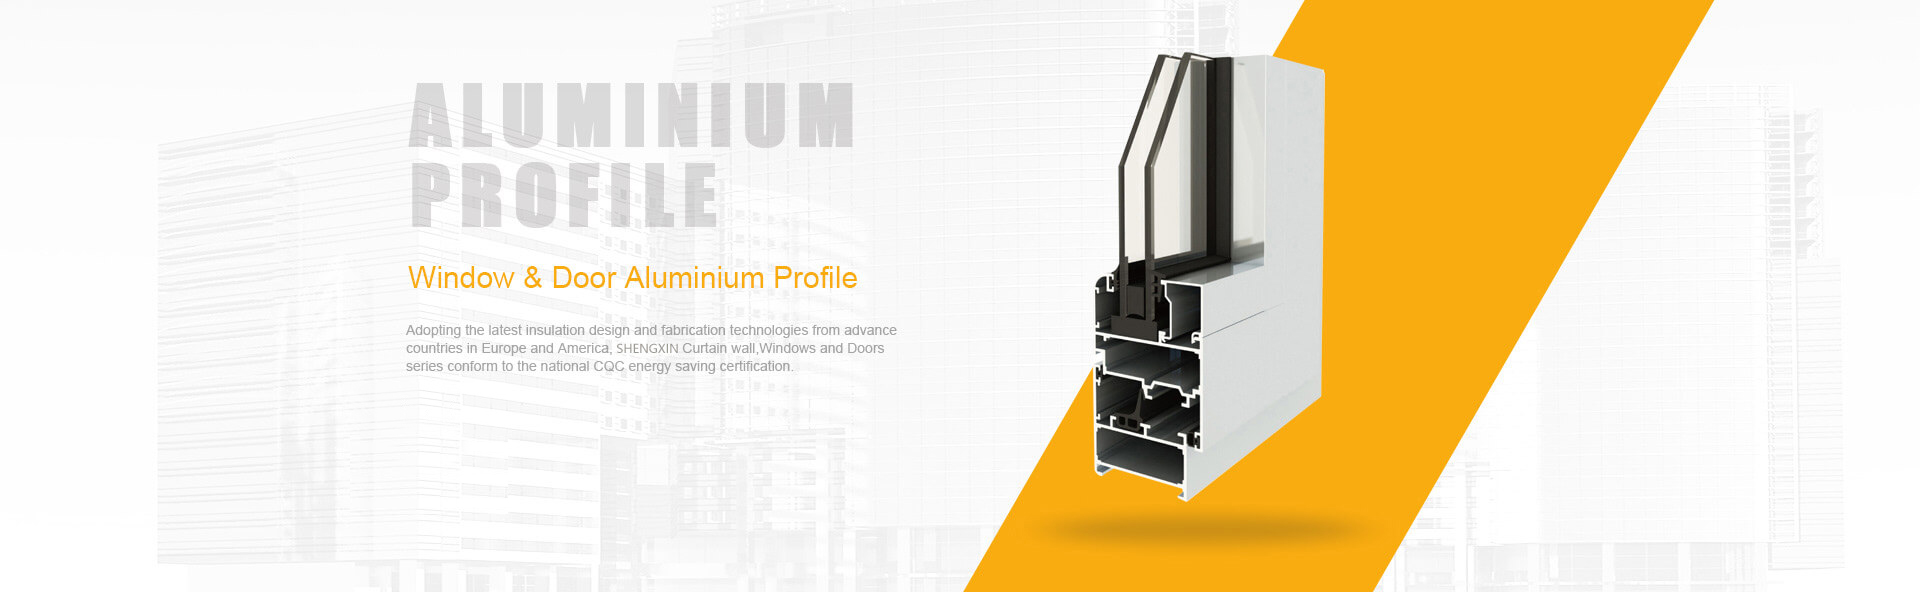
Shengxin Aluminium's deep processing services exemplify this integrated approach, offering end-to-end support that eliminates the coordination burden many exhibitors face. With 35 extrusion presses and comprehensive surface treatment facilities, such manufacturers deliver aluminium window extrusions and exhibit profiles ready for immediate assembly—no additional finishing vendors required.
When evaluating finishing capabilities, consider these factors:
The surface treatment you select ultimately determines how attendees perceive your exhibit before they ever read your messaging or examine your products. Whether you're cladding structural frameworks, finishing visible aluminium extrusion trim, or protecting outdoor installations, the right finish transforms functional aluminum into brand-aligned visual impact.
With your extrusions finished and ready for deployment, the next challenge moves from manufacturing to logistics: how do you efficiently transport, assemble, and maintain these systems across dozens or hundreds of shows?
Your aluminum extrusions are manufactured, finished, and ready. But here's the uncomfortable truth many first-time exhibitors discover too late: getting your exhibit from warehouse to show floor involves far more complexity than simply shipping boxes. Trade show logistics operate under unforgiving timelines, strict venue rules, and cost structures that punish poor planning. Let's break down the practical realities of moving modular aluminum systems efficiently.
Picture this scenario: you've got exactly four hours to transform an empty concrete floor into a polished brand environment. Union labor is on the clock. Show management is watching. Your competitors are already hanging signage. Welcome to trade show reality.
Modular aluminum extrusion assembly systems exist precisely for these pressure-cooker situations. Unlike traditional wood construction requiring skilled carpenters and extensive tooling, quality aluminum systems enable rapid deployment through standardized connections.
According to Nimlok's trade show planning experts, you should "begin I&D planning while your booth is still in the design phase." Working with your exhibit partner during design ensures your booth "will minimize on-site labor hours during assembly and teardown." This proactive approach helps avoid double-time and overtime labor costs that quickly inflate budgets.
Smart assembly strategies for aluminum extrusion kit systems include:
For portable and smaller modular displays, you may handle installation yourself—most quality aluminum systems require minimal tools and connect intuitively. However, as Nimlok notes, even self-installed booths may require union labor for specific tasks like "laying electrical wiring, rigging signs and banners." Know your venue's rules before assuming a fully DIY approach.
Freight and drayage costs catch many exhibitors off-guard. Understanding these distinct charges—and how to minimize them—directly impacts your trade show budget.
As Featherlite's logistics experts explain: "Freight gets your exhibit to the door, drayage gets it on the floor." Freight covers long-distance transportation to the venue, while drayage encompasses all material handling once your crates arrive—unloading, moving to your booth space, storing empties, and return.
Drayage is typically billed by hundredweight (CWT), making every pound count. Aluminium track extrusions and modular aluminum systems already offer significant weight advantages over wood and steel, but proper crating maximizes these savings:
For exhibits incorporating an extruded aluminum slide mechanism or other precision components, protect moving parts during transit. Foam padding, corner protectors, and custom compartments prevent the damage that derails show-morning setup.
IGE Group recommends working backward from your required arrival date to establish shipping deadlines, noting that "creating a comprehensive plan ensures your exhibit's journey goes smoothly and gives you a buffer for unexpected delays." Many shows offer advanced warehousing—allowing exhibits to arrive days early for secure storage, providing setup time buffer.
What happens to your aluminum exhibit system between events? Proper storage extends component lifespan and ensures everything remains show-ready.
Climate-controlled warehousing protects aluminum frameworks and—critically—the graphics, fabrics, and electronics that accompany them. While aluminum itself tolerates temperature extremes, attached panels and accessories may not. Storage considerations include:
Many exhibit partners offer storage programs bundled with I&D services. This streamlined approach means your exhibit ships directly from storage to venue and back—eliminating your need to coordinate multiple logistics handoffs.
Before your next event, verify every detail with this comprehensive logistics checklist:
The teardown timeline offers one final efficiency: as industry guidelines suggest, dismantling typically takes half the time of setup. Plan your return labor accordingly, but never rush packing—damaged components from careless teardown cost far more than the labor savings.
With logistics mastered, your aluminum exhibit system arrives intact and assembles efficiently show after show. But maintaining that performance over years of use requires ongoing attention—cleaning protocols, component inspection, and storage practices that extend your investment's lifespan across dozens of events.
You've invested significantly in your aluminum exhibit system. The components are engineered for durability, the finishes are professional-grade, and the modular design enables endless reconfiguration. But here's what separates exhibitors who get five years from their systems versus those achieving fifteen or more: maintenance discipline. With proper care, quality aluminum extrusions can survive hundreds of shows—but neglect accelerates wear that eventually forces costly replacements.
Let's explore the practical protocols that maximize your exhibit investment's lifespan.
Different surface treatments demand different cleaning approaches. Using the wrong products or techniques doesn't just fail to clean—it actively damages finishes that cost significant money to apply.
For powder-coated aluminum components:
According to AAMA 2604 specification guidelines, powder-coated surfaces require gentle treatment to maintain their protective properties. The general recommendation is periodic cleaning once or twice per year—but trade show environments demand more frequent attention.
Critical warning: never use strong solvents or abrasive cleaners containing trisodium phosphate, phosphoric acid, hydrochloric acid, hydrofluoric acid, or fluorides. These compounds destroy powder coating integrity irreversibly.
For anodized surfaces:
Anodized finishes integrate with the aluminum itself, making them more forgiving than powder coating—but they still require proper care. Use the same mild soap and water approach, avoiding anything abrasive. For aluminum enclosure extrusion components with anodized finishes, regular cleaning prevents buildup that becomes increasingly difficult to remove.
After every show, resist the temptation to pack everything away immediately. A systematic inspection catches problems while they're still minor repairs rather than major failures.
What to examine:
For touchup repairs on powder-coated surfaces, apply touchup paint sparingly—it's intended only for small blemishes and exposed cut ends, not large areas. Clean the repair area with denatured alcohol first to remove moisture and residue, then carefully mask surrounding areas before applying.
Connector hardware deserves special attention. These small components experience repeated stress during assembly and disassembly. Replace any fasteners showing thread wear, corner brackets with bent flanges, or T-nuts that no longer grip securely. The cost of preventive replacement is negligible compared to mid-show structural failures.
The difference between systems lasting years versus decades often comes down to handling and storage practices between events.
As exhibit lifecycle research indicates, most custom tradeshow exhibits are designed to last 5-7 years with regular care and maintenance—but "high-quality construction, professional storage, and careful shipping can stretch that lifespan even further." Paint and finish are typically "the first to wear in transit or through handling and use."
Common mistakes that shorten system lifespan:
Use this comprehensive checklist after every show to maintain peak condition:
Quality exhibit partners include refurbishment as part of their warehousing and maintenance process—inspecting components, repairing minor blemishes, and ensuring everything is show-ready before your next event. This professional maintenance cycle extends system lifespan dramatically while ensuring your brand always presents flawlessly.
With proper maintenance protocols established, your aluminum exhibit structures deliver reliable performance year after year. But when the time comes to expand your system, refresh aging components, or develop entirely new configurations, choosing the right manufacturing partner becomes critical to your long-term exhibit success.
You've mastered alloy selection, component systems, finishing options, and maintenance protocols. But here's the decision that ultimately determines whether all that knowledge translates into successful exhibits: choosing your manufacturing partner. The wrong supplier delivers delays, quality inconsistencies, and frustrating communication breakdowns. The right partner becomes a strategic asset—extending your capabilities and simplifying every project from initial concept through show floor deployment.
How do you distinguish between suppliers who merely fill orders and partners who genuinely support your exhibit ambitions? Let's build a practical evaluation framework.
Not all aluminium extrusions suppliers are created equal. The exhibit industry demands specific capabilities that general industrial suppliers may lack entirely. When evaluating potential partners, assess these critical factors:
Press Capacity and Equipment Range
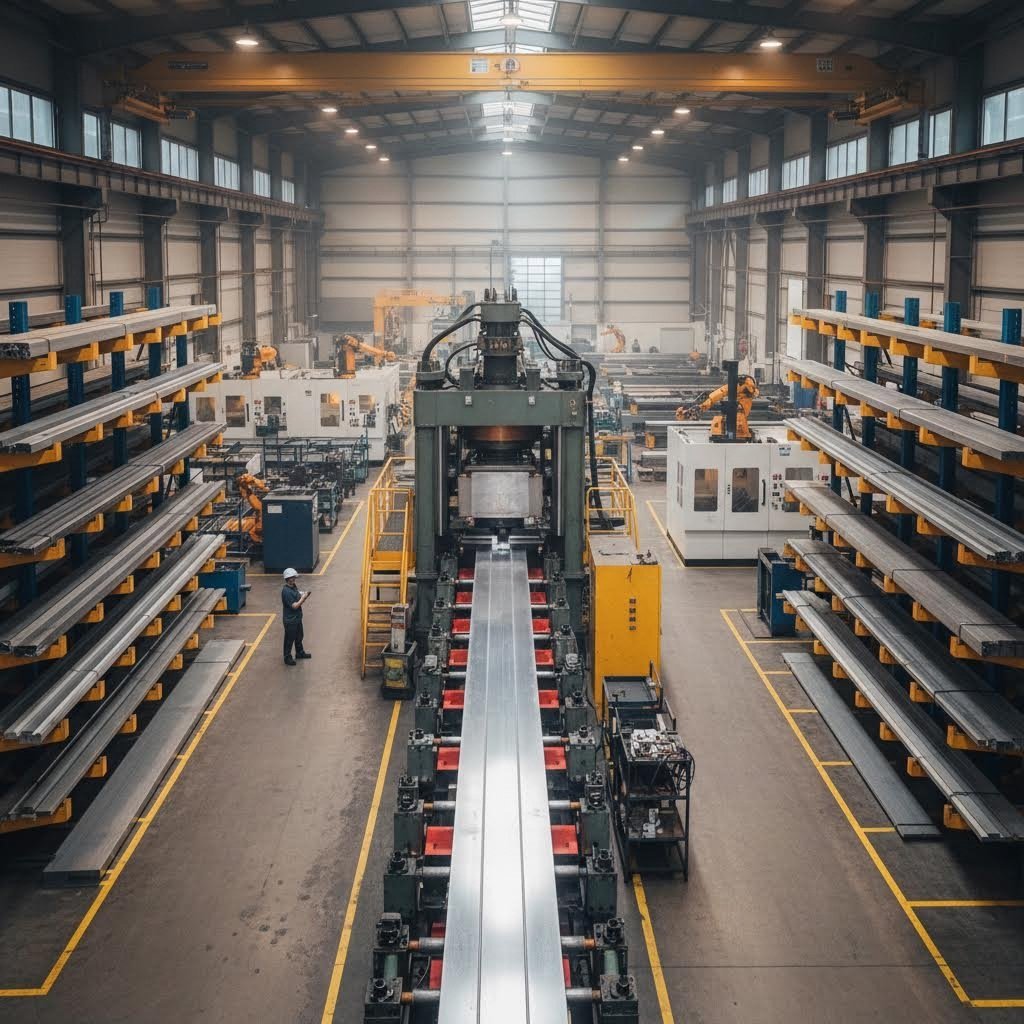
The extrusion press defines what profiles a supplier can actually produce. According to industry evaluation guidelines, press tonnage determines profile complexity and size:
Why does this matter? A supplier with multiple press capacities maintains flexibility when your project requirements vary. Your 10x10 inline booth needs different profiles than your 40x40 island installation—partnering with a manufacturer covering the full range eliminates the need for multiple supplier relationships.
Processing Services Integration
Raw extrusions rarely arrive ready for assembly. Your profiles likely require CNC cutting to precise lengths, drilling for fastener access, bending for curved elements, or complex machining for custom connections. Suppliers with integrated processing capabilities—like full CNC machining centers—deliver finished components directly to your assembly line.
As procurement experts note, "integration reduces transportation between subcontractors, prevents damage, and shortens lead time." When your extrusion, machining, and finishing happen under one roof, batch consistency in both dimension and appearance becomes achievable.
Die Design and Development Support
Custom exhibit profiles require custom dies. Many suppliers outsource die manufacturing to third parties—creating longer lead times and slower problem resolution when issues arise. Suppliers with in-house die workshops modify or repair dies quickly, ensuring production continuity.
Typical benchmarks for die development run 10-20 days, with extrusion production adding 7-15 days and surface finishing another 5-10 days. Total project timelines of 4-6 weeks are standard for custom profiles—but only with suppliers who control every step internally.
Before signing purchase orders, dig deeper with these essential questions:
Transparency during these conversations reveals whether you're dealing with a professional manufacturer or merely a trading company reselling others' production. Major U.S. distributors like CRL U.S. Aluminum provide extensive architectural product catalogs, while specialized facilities like Western Extrusion Aluminum Casting House serve specific industrial niches—understanding where your potential partner fits in the supply chain clarifies what support you can realistically expect.
The most successful exhibitors don't treat extrusion sourcing as transactional purchasing. They build relationships with manufacturing partners who understand their evolving needs.
Consider what comprehensive capability looks like in practice. Shengxin Aluminium's deep processing services exemplify the integrated approach serious exhibitors seek: 35 extrusion presses ranging from 600T to 5500T cover every profile size requirement. Full CNC machining centers handle cutting, drilling, and bending to exact specifications. Surface treatment facilities deliver anodizing in custom colors, powder coating to precise brand standards, PVDF for outdoor applications, and micro-arc oxidation for extreme durability.
This end-to-end support—from custom die development through mass production—eliminates the coordination burden that fragments projects across multiple vendors. Factory-direct relationships also provide cost advantages impossible through distribution channels, along with technical consultation that helps optimize designs before production begins.
Use this comprehensive checklist when assessing potential extrusion partners:
The exhibit industry rewards exhibitors who think strategically about their supply chain. Your aluminum extrusion partner influences not just component quality but project timelines, budget predictability, and your ability to innovate with custom designs. Choose a partner whose capabilities match your ambitions—whether that's refreshing existing systems or developing entirely new exhibit concepts that differentiate your brand on the show floor.
From alloy selection to surface treatments, component systems to logistics planning, this guide has equipped you with the comprehensive knowledge needed to make informed decisions about aluminum extrusions for your exhibit structures. The next step? Apply these insights to your upcoming projects, build relationships with capable manufacturing partners, and transform your trade show presence with the structural foundation that's become the backbone of modern exhibit design.
6063 aluminum is the most popular choice for standard exhibit frames due to its excellent extrudability and superior surface finish quality. It accepts anodizing beautifully and offers good corrosion resistance. For heavy-duty applications requiring load-bearing capacity—such as supporting large monitors or overhead signage—6061 aluminum provides higher tensile strength (310 MPa vs 270 MPa). Some manufacturers like Shengxin Aluminium offer custom extrusions in both alloys, allowing designers to combine 6063 for visible decorative elements with 6061 for structural components.
Aluminum extrusions outperform traditional materials in several key areas. They weigh approximately one-third of steel while maintaining comparable strength, significantly reducing shipping and drayage costs. Unlike wood, aluminum resists humidity damage, temperature swings, and warping—maintaining dimensional accuracy across hundreds of shows. The modular T-slot design enables infinite reconfiguration, allowing the same components to adapt to different booth sizes and layouts without specialized tools or skilled carpenters.
Aluminum extrusions accept multiple professional finishes. Anodizing creates an integral oxide layer in colors including natural silver, champagne, bronze, black, and rose gold. Powder coating enables exact Pantone or RAL color matching for brand consistency. For outdoor exhibits, PVDF coatings like Kynar provide exceptional UV and weather resistance lasting 20+ years. Specialty options include micro-arc oxidation for extreme durability and mechanical polishing for mirror-like reflectivity. Integrated manufacturers offer all treatments in-house for consistent quality.
A basic 10x10 inline booth typically requires 4-6 vertical uprights at 8-foot lengths, 3-4 horizontal rails at 10-foot lengths, and 2-4 stabilizers for cross-bracing. Venue regulations limit back walls to 8 feet maximum, with side walls stepping down to 4 feet in the front 5 feet of space. Add 10-15% contingency for cutting waste. Panel-holding extrusions depend on your graphic dimensions. For larger island configurations, requirements multiply significantly—a 20x20 island may need 8-12 perimeter uprights plus overhead framework.
Evaluate suppliers based on press capacity range (600T-5500T covers most exhibit profiles), in-house die development capability, integrated CNC machining services, and comprehensive surface treatment options. Request quality certifications like ISO 9001 and dimensional inspection documentation. Partners with end-to-end capabilities—like Shengxin Aluminium with 35 extrusion presses and full processing facilities—eliminate coordination between multiple vendors, ensuring batch consistency and shorter lead times from custom die development through finished components.


 dịch vụ trực tuyến
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Việt
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Українська