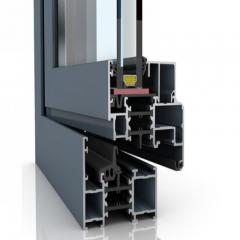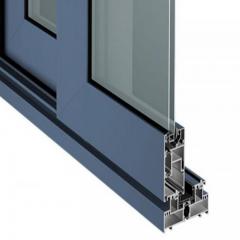
When you first start researching the cost of aluminum extrusion per pound, you'll likely stumble upon commodity prices from the London Metal Exchange (LME). You might think, "Great, aluminum is trading around $1.15 per pound—my project should be affordable!" But here's where many buyers get tripped up: the price of aluminum per pound on commodity exchanges has almost nothing to do with what you'll actually pay for finished extruded profiles.
Think of it this way: knowing the cost of aluminum per pound at the LME is like knowing the price of flour when you're trying to budget for a wedding cake. Sure, flour is a core ingredient, but the final product involves skilled labor, specialized equipment, and countless value-added steps that transform raw materials into something useful.
Aluminum extrusion pricing operates on an entirely different level than raw commodity pricing. The LME sets benchmark prices for high-purity aluminum ingots—essentially unshaped, standardized metal. But when you order custom profiles for construction, automotive, or industrial applications, you're paying for much more than just metal. You're paying for:
According to industry analysis from SinoExtrud, typical custom profiles run around $2.50 to $8.00 per kilogram (roughly $1.13 to $3.63 per pound), depending on specifications. Compare that to raw LME aluminum hovering around $2,520 per metric ton ($1.14 per pound), and you'll immediately see the disconnect.
So how much is aluminum per pound when you're actually buying extrusions? The answer depends entirely on what you need. A simple, standard profile with minimal finishing might cost only slightly more than raw material. But complex, tight-tolerance profiles with premium finishes? You could easily pay three to four times the commodity rate.
The difference between commodity aluminum and extruded profiles can be 2-4x or more depending on complexity, making it essential to understand the full cost structure rather than relying on LME benchmarks alone.
This price gap exists because extrusion is fundamentally a value-added manufacturing process. Every step from billet to finished product adds cost—and adds value. When manufacturers quote aluminum per pound for extruded profiles, they're bundling together raw material costs with regional premiums, processing overhead, labor, and any secondary operations your project requires.
Understanding this distinction is crucial for realistic budgeting. If you walk into supplier negotiations expecting LME pricing, you'll either be disappointed or, worse, fall prey to quotes that seem too good to be true. The aluminium scrap rate for recycled material follows similar patterns—even recycled aluminum carries processing costs that exceed its base commodity value.
In the sections ahead, we'll break down exactly what goes into your per-pound extrusion cost, helping you understand not just what you're paying, but why you're paying it. This knowledge empowers you to make smarter design decisions, negotiate effectively with suppliers, and ultimately get better value from every pound of aluminum you purchase.
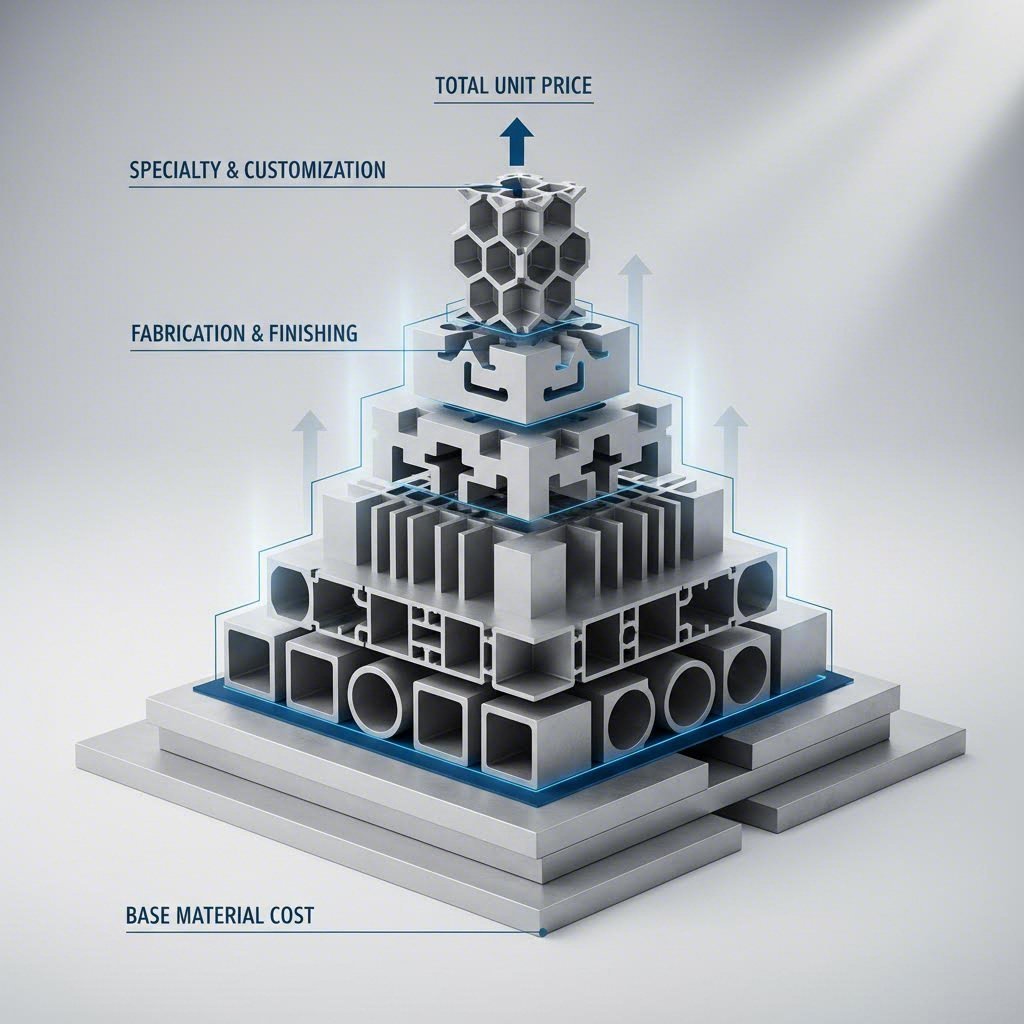
Now that you understand why extrusion pricing differs so dramatically from raw aluminum costs, let's dig into the specifics. What exactly makes up that per-pound price on your quote? When you receive pricing from a supplier, you're looking at a composite figure built from multiple cost contributors—each one adding layers to your final expense.
Understanding this breakdown transforms you from a passive quote recipient into an informed negotiator. You'll know which cost levers you can pull and which ones are fixed by market forces beyond anyone's control.
Every aluminum extrusion quote, whether you realize it or not, bundles together five distinct cost categories. Some suppliers itemize these clearly; others roll everything into a single per-pound or per-piece figure. Either way, these components exist in every transaction:
| Cost Component | What It Includes | Typical Impact on Per-Pound Price | Buyer Control Level |
|---|---|---|---|
| Raw Material Cost | LME aluminum base price + regional premium (e.g., Midwest Premium in the U.S.) | 40-60% of total cost for simple profiles | Low (market-driven) |
| Die/Tooling Cost | Custom die design, manufacturing, and maintenance—amortized across order quantity | $0.05-$1.50+ per pound depending on volume | Medium (design choices matter) |
| Extrusion Processing Cost | Press operation, labor, energy, heat treatment, stretching, cutting | 20-35% of total cost | Medium (profile complexity affects this) |
| Surface Finishing Cost | Anodizing, powder coating, painting, mechanical finishing | 15-40%+ additional cost over mill finish | High (finish selection is your choice) |
| Minimum Order Impact | Setup costs, inefficiencies, and premiums for low-volume orders | Can add 20-50%+ for orders below MOQ thresholds | High (volume planning is controllable) |
Let's walk through each component so you can see exactly how your per-pound price builds up.
Raw Material Cost: The Foundation
This is where commodity pricing enters the picture—but with a twist. Your supplier doesn't simply pay LME rates for aluminum. They pay the LME base price plus a regional premium that reflects local supply and demand dynamics. In North America, this is commonly called the Midwest Premium. According to SinoExtrud's cost analysis, raw material typically represents the largest single cost bucket, but many buyers never see how the LME price and regional premiums translate into their actual costs.
The current price of aluminum scrap also influences this component. Extruders often blend primary aluminum with recycled material to manage costs, and the aluminum scrap price fluctuates based on supply availability and quality. When aluminium scrap cost rises, it can tighten the cost advantage of using recycled content.
Die/Tooling Cost: The Custom Profile Premium
If you're ordering a standard catalog profile, you might avoid this cost entirely. But custom profiles require custom dies—steel tooling that can range from $500 for simple shapes to $5,000+ for complex multi-hollow designs. Here's the key insight: this fixed cost gets spread across your order quantity. Order 100 pounds, and a $2,000 die adds $20 per pound. Order 10,000 pounds, and that same die adds just $0.20 per pound.
Extrusion Processing Cost: Where Metal Becomes Profile
This covers everything happening on the production floor. According to IMARC Group's manufacturing analysis, the extrusion process involves heating billets to 400-500°C, forcing them through dies under tremendous pressure, then cooling, stretching, and cutting the resulting profiles. Labor, energy consumption, press time, and quality control all factor in. Complex profiles that extrude slowly or require more careful handling cost more to process than simple shapes running at high speeds.
Surface Finishing Cost: The Visible Value-Add
Mill finish—raw aluminum straight from the press—is your baseline. Every finish beyond that adds cost. Clear anodizing might add 15-25% to your per-pound price. Colored anodizing or powder coating can add 25-40% or more. These finishes deliver real value through corrosion resistance, durability, and aesthetics, but they're entirely optional. Choosing the right finish for your application (rather than defaulting to premium options) offers significant cost control.
Minimum Order Impact: The Small-Batch Penalty
Every extrusion run involves setup time, die changes, and quality verification—costs that exist whether you order 50 pounds or 5,000 pounds. Suppliers set minimum order quantities (MOQs) to ensure these fixed costs don't consume their margins. Fall below the MOQ threshold, and you'll typically pay a premium. Some suppliers quote per-pound prices that look attractive but hide setup fees or small-order surcharges in the fine print.
What's often missing from competitor resources—including those that mention LME pricing and regional premiums—is this practical translation into buyer-facing costs. Knowing that aluminum trades at a certain price per pound tells you almost nothing about what you'll actually pay. Similarly, understanding scrap steel rate or salvage steel price trends might inform recycled metal markets, but aluminum extrusion pricing follows its own dynamics shaped by these five interconnected components.
Armed with this breakdown, you can now ask smarter questions when reviewing quotes. Request itemized pricing. Understand where your money goes. And most importantly, identify which cost components you can influence through design decisions, volume commitments, or finish selections. In the next section, we'll explore how your alloy choice—often an overlooked decision—can significantly shift your per-pound costs up or down.
You've chosen aluminum extrusion for your project—great decision. But here's a question that can swing your per-pound cost by 30% or more: which alloy are you specifying? Many buyers default to whatever their supplier suggests without realizing that alloy selection represents one of the most controllable cost levers in the entire extrusion process.
Think of aluminum alloys like grades of lumber. You wouldn't use exotic hardwood for warehouse shelving, and you wouldn't build fine furniture from construction-grade pine. The same logic applies here. Matching alloy properties to your actual application requirements—rather than over-specifying "just to be safe"—can save significant money without sacrificing performance.
Aluminum extrusion alloys aren't created equal, and neither are their price tags. The 6000 series dominates the extrusion market because these alloys offer an excellent balance of strength, corrosion resistance, and extrudability. But within this series—and across others—meaningful cost and performance differences exist.
According to TBK Metal's 2025 aluminum cost guide, pricing varies significantly by grade. The 6061 aluminum price per pound runs notably higher than 6063 due to its enhanced strength characteristics. Meanwhile, premium alloys like 7075 can cost nearly double what you'd pay for standard architectural grades.
Why the variation? Three factors drive alloy pricing:
The extruded aluminum scrap price also varies by alloy grade. When you're evaluating total lifecycle costs, remember that clean extruded aluminum scrap price for 6063 architectural profiles typically commands better recycling value than mixed or specialty alloys—a factor worth considering for sustainability-focused projects.
Let's put real numbers and characteristics side by side. This comparison covers the most commonly specified extrusion alloys, helping you match requirements to the most cost-effective option:
| Alloy | Typical Applications | Relative Cost Factor | Extrudability Rating | Key Considerations |
|---|---|---|---|---|
| 6063 | Window frames, curtain walls, decorative trim, lighting fixtures | 1.0x (baseline) | Excellent | Best surface finish; most economical for architectural work |
| 6061 | Structural frames, marine components, automotive parts, machinery | 1.15-1.25x | Good | Higher strength; poorer finish response than 6063 |
| 6005 | Ladders, platforms, building construction, marine applications | 1.10-1.20x | Excellent | Strength between 6063 and 6061; good all-around choice |
| 6463 | Automotive trim, shower enclosures, picture framing | 1.20-1.30x | Good | Premium bright finish; ideal for decorative applications |
| 7075 | Aerospace components, high-stress structures, specialized tooling | 1.8-2.2x | Poor | Exceptional strength; limited formability; higher scrap rates |
Notice that 6063 serves as the cost baseline—it's often called the "architectural alloy" because it delivers excellent surface finish at the lowest price point. According to Tri-State Aluminum's alloy guide, 6063 is the most cost-efficient choice for architectural applications, offering good corrosion resistance alongside solid machinability and formability.
The 6061 aluminum price per pound runs 15-25% higher, but this premium buys you meaningfully better mechanical strength. If your application involves load-bearing structures or requires superior machining characteristics, that extra cost delivers real value. However, 6061's poorer finishing response means it's less ideal for consumer-facing surfaces where aesthetics matter.
Sounds straightforward—just pick the cheapest alloy that works, right? Not quite. Underspecifying can cost you more in the long run through premature failure, safety issues, or expensive redesigns. Here's when paying more makes sense:
Conversely, specifying 6061 for interior architectural trim or 7075 for non-structural components wastes money without adding value. Many buyers overspecify because they're unfamiliar with alloy options—or because a supplier defaults to higher-margin materials.
The aluminum extrusion scrap prices for different alloys also affect your total cost picture. Higher-grade alloys like 7075 generate more expensive scrap, but their poor extrudability often means higher scrap rates during production—a hidden cost that factors into per-pound pricing.
Before finalizing your alloy selection, ask yourself: What strength does my application actually require? Does the surface finish matter for end users? Will this component face corrosive environments? Honest answers often point toward more economical options than initial assumptions suggest. With alloy selection clarified, the next major cost driver to understand is profile complexity—how the shape itself influences what you'll pay per pound.
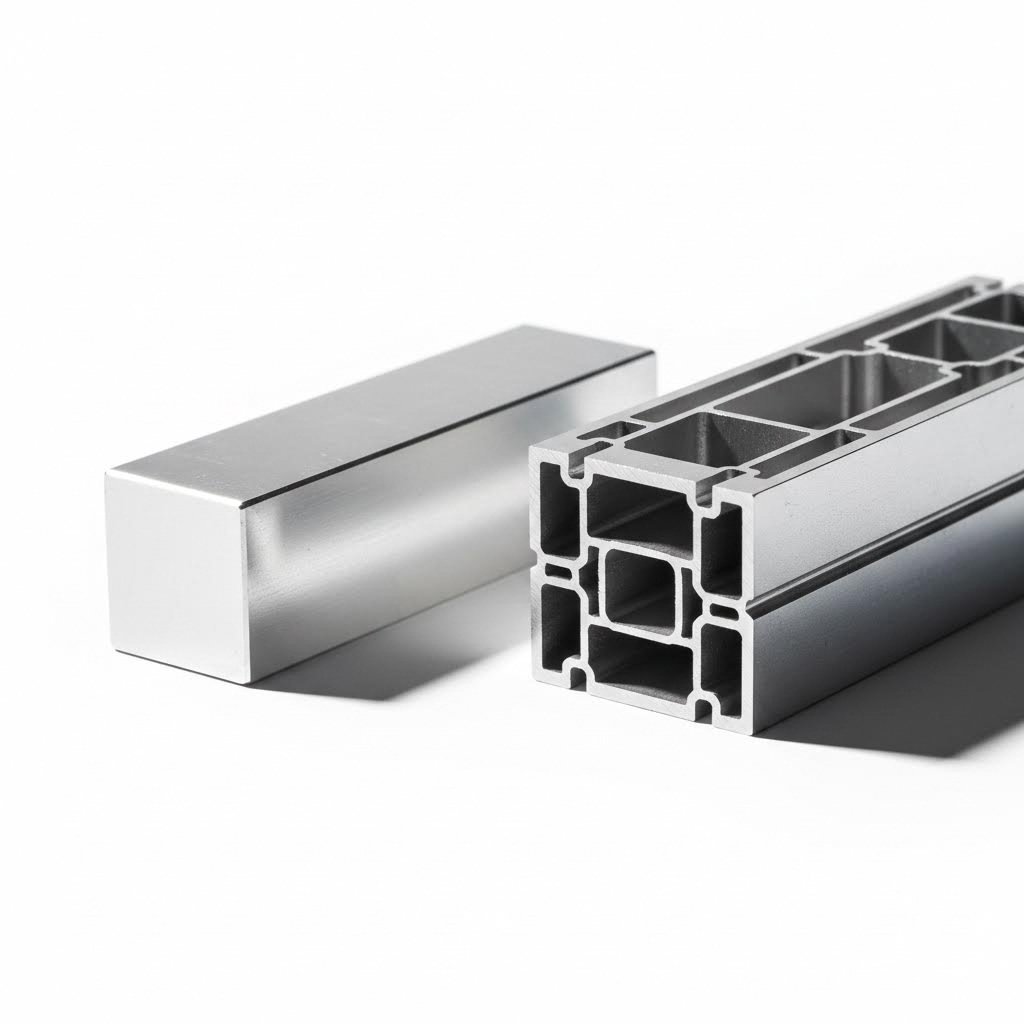
You've selected your alloy. Now comes a decision with even greater cost implications: your profile's geometry. The shape you design—its complexity, wall thickness, and tolerance requirements—can swing your per-pound price by 50% or more. Yet many buyers treat profile design as purely an engineering exercise, missing opportunities to optimize costs without sacrificing functionality.
Imagine two profiles using identical 6063 aluminum. One is a simple rectangular tube; the other features multiple hollows, thin walls, and asymmetrical geometry. Same material, dramatically different costs. Understanding why helps you make smarter design decisions from the start.
Every added complexity in your profile design ripples through the manufacturing process, affecting die construction, extrusion speed, scrap rates, and quality control requirements. According to American Douglas Metals' extrusion design guide, raw material expenses constitute 90% of basic extrusion costs—but that percentage shrinks significantly as profile complexity increases, with processing and tooling absorbing larger shares.
Here are the primary complexity factors that drive up your per-pound pricing:
Solid vs. Hollow Profiles: The Cost Gap
The distinction between solid and hollow profiles represents one of the most significant cost differentials in extrusion. According to Profile Precision Extrusions, custom dies typically range from $1,250 to $1,950, with solid dies being "simpler and more affordable" than hollow alternatives.
Why the difference? Hollow aluminium extrusion dies require porthole or bridge construction—complex internal structures that shape the hollow cavities while allowing metal to flow around and rejoin. These dies:
If your design can achieve its functional requirements with a solid profile—or with fewer hollows—you'll see meaningful cost savings across tooling, processing, and quality control.
Wall Thickness: The Speed and Scrap Equation
Wall thickness affects your cost through two interconnected mechanisms: extrusion speed and scrap generation. Thinner walls extrude more slowly because the metal must be carefully controlled to prevent defects. They also cool more rapidly than thick sections, creating dimensional control challenges.
According to the American Douglas Metals guide, maintaining balanced wall thickness delivers several advantages: faster production cycles, enhanced dimensional precision, improved surface uniformity, and better profile consistency. When adjacent wall thickness ratios exceed 2:1, dimensional control becomes significantly more challenging—and expensive.
Practical guidelines for wall thickness optimization:
Here's a question that can save—or waste—significant money: Do you actually need those tight tolerances you're specifying?
According to SinoExtrud's tolerance analysis, tighter tolerances increase costs because achieving them demands more precise tooling, slower machine speeds, more die maintenance, higher scrap rates, and more inspection. Every factor adds time and expense.
Standard commercial tolerances exist for good reason—they represent the dimensional accuracy achievable through normal extrusion processes without special measures. Moving beyond these standards triggers a cascade of cost-adding requirements:
Where Tolerance Problems Typically Occur
Certain profile features are inherently harder to hold within tolerance. Understanding these trouble spots helps you focus tight tolerance requirements only where they genuinely matter:
Practical Guidance: Optimizing Design for Cost
How do you balance cost optimization with functional requirements? Start by questioning every complexity in your design:
Custom aluminum extrusions don't have to be expensive. Understanding how aluminum extrusion is made—and where complexity adds cost—empowers you to design profiles that meet functional requirements without unnecessary manufacturing premiums. The key lies in making informed trade-offs rather than defaulting to over-engineered specifications.
With profile complexity understood, another often-misunderstood aspect of extrusion pricing awaits: the different pricing models suppliers use and how to navigate them effectively.
You've requested quotes from three suppliers, and now you're staring at numbers that seem impossible to compare. One quotes $2.85 per pound, another offers $1.45 per foot, and the third prices at $12.50 per piece. Which one is actually the best deal? Without understanding these different pricing models, you're essentially comparing apples to oranges—and potentially leaving money on the table.
Here's something most suppliers won't tell you: the pricing model they use often reflects their business focus more than your project's needs. Understanding when each model applies—and how to convert between them—transforms confusing quotes into actionable intelligence.
The aluminum extrusion industry uses three primary pricing structures, each with distinct advantages depending on your project characteristics. According to TigerStop's manufacturing analysis, it's standard to buy aluminum extrusions by the linear foot rather than by weight—yet scrap is sold by the pound. This disconnect hints at the complexity buyers face when evaluating extruded aluminum prices across different quoting conventions.
| Pricing Model | Best Suited For | Advantages | Watch-Outs |
|---|---|---|---|
| Per Pound | Commodity profiles, heavy cross-sections, large volume orders where weight is the primary cost driver | Easy comparison across suppliers; transparent material cost basis; scales predictably with order size | Doesn't reflect processing complexity; lightweight profiles appear expensive; harder to estimate project totals |
| Per Foot | Consistent cross-sections, architectural applications, projects measured in linear quantities | Direct correlation to project needs; simple quantity calculations; easier budgeting for construction projects | Hides weight-based cost variations; complex profiles may be underpriced relative to true cost; finish costs often excluded |
| Per Piece | Complex fabricated parts, cut-to-length components, assemblies with secondary operations | All-inclusive pricing simplifies budgeting; accounts for fabrication complexity; reduces surprise costs | Difficult to compare across suppliers; may obscure per-pound or per-foot base rates; less flexibility for quantity changes |
When Per-Pound Pricing Makes Sense
Per-pound pricing dominates commodity extrusion markets because it directly reflects the primary cost driver: aluminum itself. When you're ordering standard profiles with minimal finishing—think structural angles, channels, or basic tubing—the price of 1 pound of aluminum correlates closely with your total cost. This model works well for heavy-gauge profiles where material consumption represents the largest expense category.
However, per-pound quotes can mislead when comparing lightweight, complex profiles. A thin-walled architectural profile might weigh half as much per foot as a solid bar, yet require significantly more processing expertise and die sophistication. Quoting both at the same per-pound rate would dramatically undervalue the complex profile's true manufacturing cost.
When Per-Foot Pricing Works Better
Architectural and construction projects typically think in linear measurements—how many feet of window framing, how many meters of curtain wall mullion. Per-foot pricing aligns supplier quotes with project takeoffs, making budget estimation straightforward.
This model also normalizes comparison across profiles with different weights. A quote of $1.45 per foot tells you exactly what 100 feet costs, regardless of whether the profile weighs 0.5 or 1.5 pounds per foot. For consistent cross-sections running through a project, per-foot pricing eliminates mental math.
When Per-Piece Pricing Delivers Clarity
Complex fabricated parts—cut to length, drilled, bent, or assembled—involve too many variables for simple per-pound or per-foot quotes to capture accurately. Per-piece pricing bundles extrusion, finishing, fabrication, and quality control into a single number that represents your true delivered cost.
This model proves especially valuable when secondary operations add substantial value. If your component requires precision cutting, CNC machining, and specialized packaging, a per-piece quote prevents the unpleasant surprise of fabrication charges arriving separately.
So how do you request quotes that enable genuine comparison? Start by understanding your project's primary characteristics:
Converting Between Pricing Models
When suppliers quote in different formats, you'll need to convert for accurate comparison. The key variable is weight per linear foot—a specification any supplier should provide. Here's how the math works:
Remember that per-piece pricing often includes value-added operations, so direct conversion to per-foot rates may understate the base extrusion cost. Always ask suppliers to itemize fabrication charges when possible.
The scrap aluminum price per pound follows similar unit conventions—recyclers pay by weight regardless of original profile geometry. Understanding that the price of one pound of aluminum scrap hovers around $0.50 (versus $2.50+ for new extrusions, as noted in TigerStop's analysis) reinforces why minimizing waste matters more than chasing marginally lower per-pound quotes.
Armed with the ability to translate between pricing models, you're ready to tackle another often-misunderstood cost component: die tooling and how it amortizes across your order quantity.
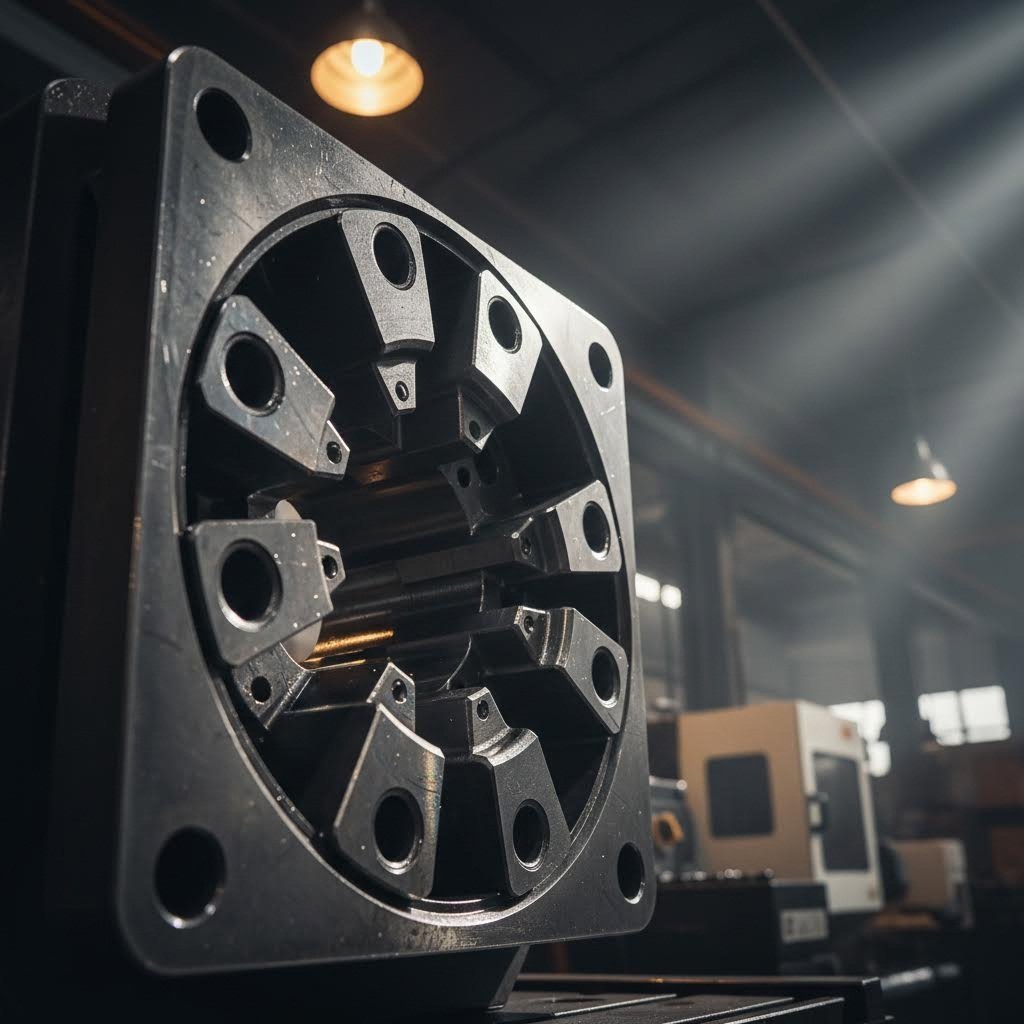
Here's a cost that catches many first-time buyers off guard: before a single pound of aluminum flows through your custom profile, someone has to build the die that shapes it. This tooling investment—separate from your per-pound extrusion cost—can range from a few hundred dollars to several thousand. And how that cost spreads across your order quantity dramatically affects what you're really paying per pound.
Think of extrusion dies like custom cake pans. A bakery using the same pan hundreds of times barely notices the original purchase cost. But if you're ordering just one specialty cake? That pan's price becomes a significant part of your total bill. The same math applies to aluminium extrusion tooling—and understanding it can save you thousands.
Extrusion dies are precision-machined steel tools that shape heated aluminum billets into specific cross-sectional profiles. According to Shao-Yi's analysis of extrusion die ROI, die costs typically range from $300 for simple solid profiles to over $2,000 for intricate hollow designs—with highly complex multi-void profiles potentially exceeding $5,000.
What drives these cost variations? Several interconnected factors determine what you'll pay for aluminium extrusion dies:
Understanding Die Type Cost Ranges
The type of aluminum extrusion die you need depends entirely on your profile geometry. Here's how costs typically break down:
| Die Type | Structure | Typical Cost Range | Common Applications |
|---|---|---|---|
| Solid Die | One-piece construction, no bridges or mandrels | $300–$800 | Angles, channels, flat bars, simple shapes |
| Semi-Hollow Die | Narrow openings with partial bridge structures | $800–$1,500 | Mounting brackets, clips, specialized trim |
| Hollow Die | Full mandrel and bridge assembly | $1,000–$3,000 | Tubes, square sections, window frames |
| Multi-Cavity Die | Multiple identical cavities in single die | $1,500–$5,000+ | LED housings, heat sink fins, high-volume small parts |
Die Ownership: Who Keeps the Tooling?
Die ownership policies vary by supplier—and they matter more than most buyers realize. Some extruders retain die ownership, storing your tooling for reorders but charging again if you switch suppliers. Others transfer ownership to you after the initial order, giving you flexibility to move production elsewhere.
Before committing, clarify these questions:
Here's where the math gets interesting—and where many buyers either overspend or miss opportunities. The key question isn't "How much does the die cost?" but rather "How does die cost affect my per-pound price at my expected order volume?"
Amortization: The Volume Game
Die cost is fixed. Whether you order 100 pounds or 100,000 pounds, that $1,500 aluminum extrusion die costs exactly the same. But its impact on your per-pound price changes dramatically based on how many pounds you spread it across:
According to Shao-Yi's ROI analysis, at high volumes the die cost "approaches zero" as a factor in per-unit pricing—making custom aluminium extrusions remarkably economical for mass production compared to processes like die casting, where tooling can exceed $25,000.
Standard Catalog Profiles: The Die-Free Alternative
What if you could skip die costs entirely? You can—by selecting from a supplier's existing catalog of standard profiles. These common shapes (rectangular tubes, angles, channels, T-sections) use dies that were amortized long ago across countless orders.
Standard profiles offer immediate advantages:
The trade-off? You're limited to available geometries. If a catalog profile meets your functional requirements—even if it's not a perfect match—the cost savings often outweigh minor design compromises.
MOQ Thresholds: The Small-Order Penalty
Minimum order quantities exist because extrusion runs involve significant setup regardless of order size. Die changes, press calibration, temperature stabilization, and first-article inspection happen whether you're making 50 pounds or 5,000 pounds.
According to XiHui Aluminum's industry analysis, typical MOQs run around 500 kg (approximately 1,100 pounds) per design. Orders below this threshold trigger one of two outcomes:
For buyers placing smaller orders, this MOQ dynamic can devastate your per-pound economics. A profile that costs $3.00 per pound at 2,000 pounds might effectively cost $5.00 or more at 200 pounds once die amortization and small-lot fees are factored in.
Strategic Approaches for Small-Volume Buyers
If your quantities fall below typical MOQ thresholds, consider these strategies:
Understanding die economics separates informed buyers from those who get surprised by tooling charges or wonder why their small orders cost so much more per pound. But tooling is just one piece of the puzzle—surface finishing represents another significant cost layer that many quotes don't fully explain upfront.
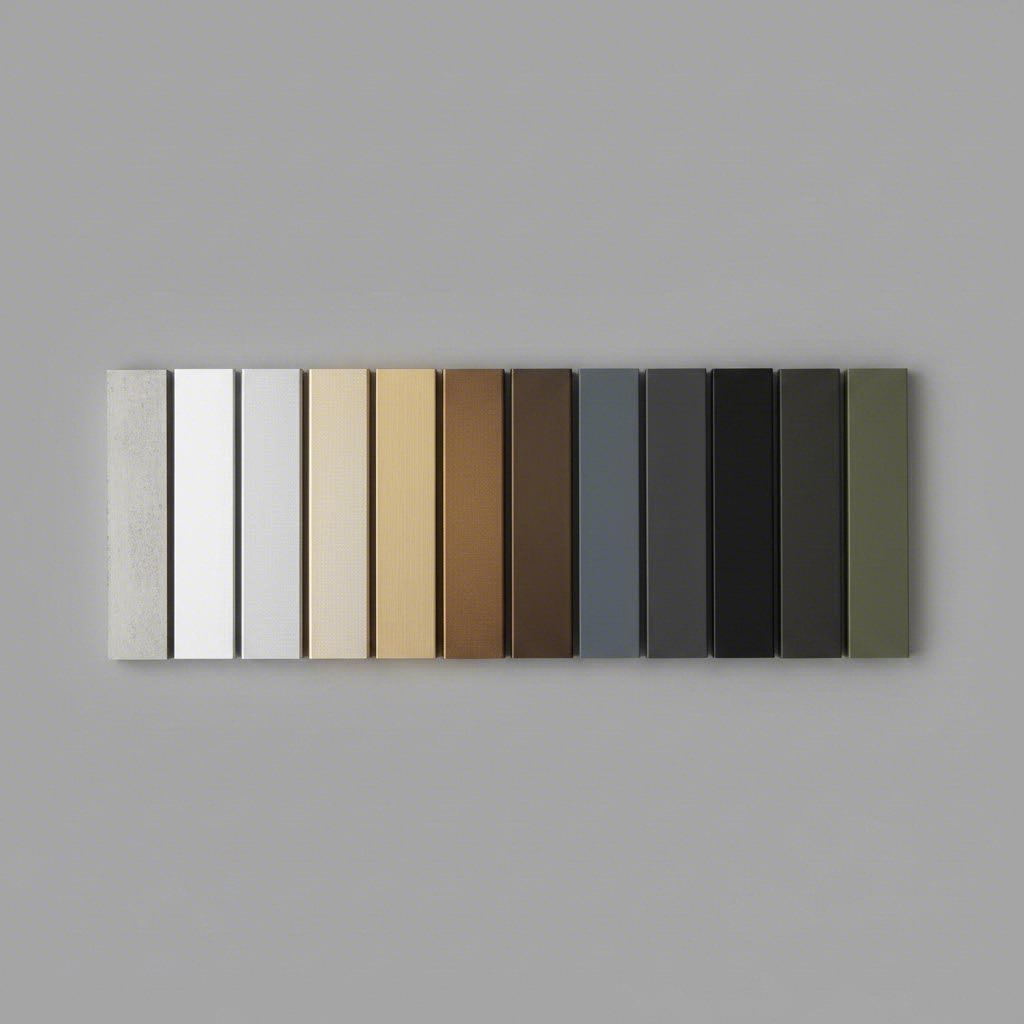
You've selected your alloy, optimized your profile design, and negotiated favorable die terms. Now comes a decision that can add anywhere from 5% to 50% to your per-pound cost: surface finishing. For some applications, this investment delivers tremendous value. For others, it's money you don't need to spend.
Here's what many buyers don't realize: finishing costs aren't just about aesthetics. The right surface treatment extends component life, reduces maintenance, and can actually lower total ownership costs—even when it raises your initial per-pound price. The wrong finish? That's money wasted on performance you'll never need.
Surface treatments transform raw extruded aluminum into finished components ready for their intended application. According to Ya Ji Aluminum's 2025 cost analysis, surface treatment typically represents 5-15% of total extrusion cost—but premium finishes can push this significantly higher depending on specifications and order volume.
Let's break down what each option adds to your per-pound pricing:
| Finish Type | Relative Cost Factor | Added Cost Per Pound | Typical Applications | Key Benefits |
|---|---|---|---|---|
| Mill Finish | 1.0x (baseline) | $0.00 | Industrial components, hidden structures, parts receiving secondary coating | Lowest cost; fastest delivery; suitable for non-visible applications |
| Clear Anodizing | 1.15-1.25x | $0.10-$0.30/kg ($0.05-$0.14/lb) | Architectural trim, electronics housings, marine hardware | Enhanced corrosion resistance; maintains natural aluminum appearance; electrically insulating |
| Colored Anodizing | 1.25-1.40x | $0.15-$0.40/kg ($0.07-$0.18/lb) | Consumer electronics, sporting goods, decorative fixtures | Vibrant, fade-resistant colors; integral to surface (won't peel); excellent wear resistance |
| Powder Coating | 1.25-1.50x | $0.20-$0.50/kg ($0.09-$0.23/lb) | Outdoor furniture, building facades, automotive components | Wide color range; excellent impact resistance; thicker protective layer than anodizing |
| PVDF Coating | 1.50-2.00x | $0.50-$1.00+/kg ($0.23-$0.45+/lb) | Architectural curtain walls, storefronts, high-end building exteriors | Superior UV resistance; 20+ year color retention; industry-leading weatherability |
| Specialty Finishes | 1.75-2.50x+ | $0.60-$1.50+/kg ($0.27-$0.68+/lb) | Premium architecture, wood-grain effects, electrophoretic coatings | Unique aesthetics; specialized performance properties; distinctive market positioning |
Understanding Anodizing Cost Factors
Anodizing isn't a coating—it's an electrochemical process that converts the aluminum surface into a durable oxide layer. According to PTSMAKE's comprehensive finishing guide, anodizing typically adds 5% to 15% to the total cost of a CNC machined part, with final pricing depending on anodizing type, coating thickness, part size, and batch quantity.
Type II (decorative) anodizing creates thinner layers suitable for aesthetic applications, while Type III (hardcoat) anodizing produces much denser, wear-resistant surfaces—at correspondingly higher cost. For profiles requiring masking to keep certain areas free of anodizing, expect labor-intensive manual work that adds considerable expense.
Powder Coating vs. Anodizing: The Trade-Off
Both finishes offer excellent protection, but they serve different needs. Anodizing integrates with the aluminum surface—it can't peel or chip because it literally becomes part of the metal. Powder coating sits atop the surface, offering thicker protection and better impact resistance but remaining vulnerable to adhesion failure if improperly applied.
For stainless steel price comparisons, note that aluminum with quality finishing often competes favorably against stainless on a cost-per-pound basis while offering significant weight advantages. The stainless steel price per pound typically runs 3-5x higher than finished aluminum extrusions, making aluminum an attractive alternative for weight-sensitive applications.
PVDF: The Premium Standard for Architecture
When longevity and color retention matter most, PVDF (polyvinylidene fluoride) coatings deliver unmatched performance. According to Sherwin-Williams' PVDF coating guide, 70% PVDF resin-based coatings have become "one of the most popular and respected coil and extrusion coatings available on the market" over the past half-century.
What justifies PVDF's premium pricing? Carbon-fluorine bonds—among the strongest chemical bonds available—give these coatings stubborn resistance to chalking, fading, and atmospheric pollutants. Real-world testing demonstrates that properly applied PVDF coatings maintain color integrity for 20+ years, even under harsh UV exposure.
So when does premium finishing justify its cost? Consider these scenarios:
Conversely, mill finish often makes perfect sense:
When evaluating stainless steel scrap price versus aluminum scrap value, remember that finished aluminum extrusions retain recycling value regardless of surface treatment—though stainless scrap price and scrap price of stainless typically command higher rates due to material composition. However, the initial cost advantage of aluminum often outweighs end-of-life scrap considerations.
Surface finishing can add 15-50% to your per-pound cost, but for architectural and consumer-facing applications, the right finish often pays for itself through extended service life, reduced maintenance, and enhanced product value.
The key lies in matching finish performance to actual application requirements—not defaulting to premium options "just in case" or cutting corners where appearance and durability genuinely matter. With finishing economics understood, you're now ready to navigate the quote process itself—learning how to request accurate pricing and spot red flags that signal trouble ahead.
You've done your homework. You understand alloy options, profile complexity factors, and surface finishing costs. Now comes the moment of truth: requesting actual quotes from suppliers. This step trips up more buyers than any other—not because the process is inherently difficult, but because incomplete requests lead to incomplete quotes, making accurate comparison nearly impossible.
Here's what separates buyers who get reliable pricing from those who face surprise charges later: preparation and specificity. The more complete your request, the more accurate your quote. And the more itemized that quote, the better you can identify where your money actually goes.
Think of your quote request like a recipe handoff to a chef. Vague instructions—"make something with chicken"—yield unpredictable results. Detailed specifications—exact ingredients, cooking methods, presentation requirements—deliver exactly what you envisioned. According to Profile Precision Extrusions, quote turnaround for simple designs can happen within 24 hours, while complex extrusions may take 72 hours—but only when buyers provide complete information upfront.
Follow this step-by-step process to ensure your quote requests generate comparable, reliable pricing:
Why Comprehensive Capabilities Matter for Quote Accuracy
Here's something that often goes unmentioned: suppliers with integrated capabilities—extrusion, finishing, and fabrication under one roof—typically provide more accurate all-in pricing than those who subcontract secondary operations. When aluminum extrusion tooling, CNC machining, and surface treatment happen at different facilities, coordination gaps create pricing uncertainty.
Established custom aluminum extruders with deep processing capabilities can quote the complete cost of your finished component, not just the raw extrusion. This matters because fabrication and finishing often represent 30-50% of total part cost. For example, Shengxin Aluminium offers end-to-end support from die development through mass production, with in-house CNC machining and multiple surface treatment options—enabling comprehensive quotes that account for every processing step.
Not all quotes deserve equal consideration. According to industry guidance on manufacturer selection, certain warning signs indicate potential problems ahead. Watch for these red flags when evaluating custom aluminium extrusion quotes:
Comparing Quotes Effectively
Once quotes arrive, resist the urge to simply pick the lowest number. Instead, normalize pricing to enable genuine comparison:
According to Gabrian International's cost analysis, selecting a manufacturer with vertically integrated capabilities "will minimize the burden of logistical management and reduce the final cost for your order when compared with completing coordinated operations between multiple different vendors." This integration advantage often outweighs modest per-pound price differences.
The quote process reveals more than just pricing—it demonstrates supplier professionalism, communication quality, and attention to detail. Suppliers who provide thorough, transparent quotes typically deliver the same care throughout production. Those who cut corners during quoting rarely improve later.
With quotes in hand and red flags identified, you're ready to make an informed supplier decision. The final step is synthesizing everything you've learned about extrusion costs into a coherent purchasing strategy that balances price, quality, and long-term value.
You've now explored every layer of what determines the cost of aluminum extrusion per pound—from raw material economics to die amortization, from alloy selection to surface finishing premiums. But knowledge without action is just trivia. So how do you translate this understanding into smarter purchasing decisions that save money without sacrificing quality?
The answer lies in prioritizing the factors that matter most for your specific project while remaining flexible on elements that don't significantly impact performance. Let's synthesize everything into actionable guidance you can apply immediately.
When evaluating what you're really paying for, four cost drivers demand your primary attention:
Understanding the complete cost structure—not just the headline per-pound price—enables better supplier negotiations and realistic budgeting. Buyers who grasp how each component contributes to total cost consistently achieve 10-20% better outcomes than those who simply chase the lowest quote.
So what's the scrap price of aluminum versus finished extrusions? Recycled aluminum typically trades around $0.40-$0.60 per pound, while finished extrusions run $2.50-$8.00 or more. That gap—representing value added through processing, finishing, and precision manufacturing—explains why focusing solely on raw material prices leads buyers astray.
Here's how to balance cost optimization with quality requirements:
Why Integrated Capabilities Matter
For buyers seeking custom extrusions with competitive pricing, supplier capabilities extend beyond just the extrusion press. When ss steel price and ss material price comparisons enter your evaluation—perhaps considering stainless alternatives—aluminum's weight advantage and lower processing costs often prove decisive. But realizing those advantages requires suppliers who can deliver complete solutions.
Suppliers with extensive press capacity and in-house finishing capabilities offer meaningful advantages in both pricing and lead times. They eliminate coordination overhead between multiple vendors, reduce quality variability from handoffs, and provide single-point accountability for your complete order.
Consider what comprehensive capability looks like in practice: Shengxin Aluminium operates 35 extrusion presses ranging from 600T to 5500T capacity, paired with in-house CNC machining and comprehensive surface treatment options including anodizing, powder coating, and PVDF. This integration enables factory-direct pricing without the markup layers that accumulate when multiple specialists handle different production stages.
What's the price for aluminum scrap versus the value you're creating? That question matters less than understanding how much is aluminium worth as a finished, application-ready component. When you find suppliers who streamline the path from raw billet to completed profile, the total value equation shifts decisively in your favor.
Armed with the knowledge from this guide, you're now equipped to request accurate quotes, compare suppliers meaningfully, and negotiate from a position of genuine understanding. The cost of aluminum extrusion per pound isn't a mystery—it's a calculation you can now perform with confidence.
Primary aluminum trades around $1.17 per pound on commodity exchanges, but this reflects raw material only. Finished aluminum extrusions typically cost $2.50 to $8.00 per pound depending on alloy grade, profile complexity, and surface finishing requirements. The gap between commodity pricing and extrusion costs accounts for processing, tooling, labor, and value-added operations that transform raw billets into usable profiles.
Clean 6063 aluminum extrusion scrap typically trades between $0.80 and $0.95 per pound, making it one of the more valuable aluminum scrap grades due to its purity and recyclability. Architectural-grade 6063 often commands better scrap prices than mixed alloys because recyclers can more easily reprocess it into new extrusions without extensive alloy adjustments.
Extracting primary aluminum from bauxite ore costs approximately $1,660 per metric ton through mining and smelting processes. However, recycling aluminum extrusions costs significantly less—roughly 5% of the energy required for primary production. This makes recycled aluminum content an attractive cost-reduction strategy for manufacturers while maintaining material quality.
Four factors dominate custom extrusion costs: alloy selection (6063 costs 15-25% less than 6061), profile complexity (hollow sections require more expensive dies), order quantity (die costs spread across volume), and surface finishing (PVDF coating can double finishing expenses). Understanding these drivers helps buyers optimize designs and negotiate effectively with suppliers like Shengxin Aluminium, which offers integrated extrusion and finishing services.
Quote variations stem from differences in pricing models (per-pound vs. per-foot vs. per-piece), included scope (some exclude tooling or finishing), supplier capabilities, and regional cost structures. Integrated suppliers with in-house extrusion, CNC machining, and surface treatment—such as those operating multiple press lines—often provide more accurate all-in pricing because they control the entire production chain without subcontracting markups.


 dịch vụ trực tuyến
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 Việt
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 ไทย
 Українська